Posted by McKenzie Thorpe on | Comments Off on How to Fight Hidden Air in Hydraulic Tanks
Your reservoir is more than just a holding space for hydraulic fluid.
“If the reservoir isn’t leaking, all is well, right?”
Actually, the hydraulic tank assembly plays a critical role in removing damaging air contamination from your fluid!
Despite being the central pillar of controlling air contamination, many reservoirs aren’t well-optimized for the job. Even reservoirs that perform adequate deaeration might be secretly weighing down the system and the oil budget.
How can air contamination affect my hydraulic system?
Discussions around contamination usually focus on solid particulates and water. But what happens to a hydraulic system when it becomes contaminated by air?
If not controlled, air contamination targets system components, overall oil condition, and machine efficiency:
Accelerated Oil Aging: Oxygen in the air speeds up the aging of oil.
Varnish / Gel-Like Buildup: Oil aging byproducts like varnish can foul and damage hydraulic system components.
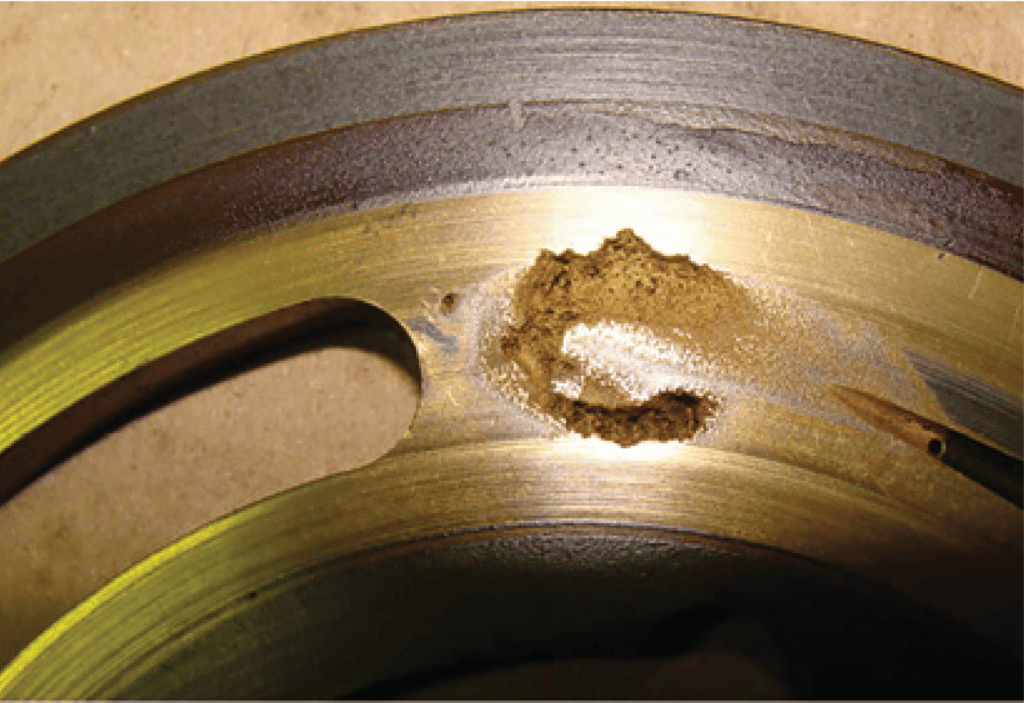
Cavitation: Air bubbles can collapse so violently under high pressure that physical damage occurs.
Microdieseling: Air bubbles may also combust under high pressure, literally burning the surrounding oil & speeding up aging and byproduct formation.
‘Spongy’ Hydraulics: Compressible air can cause delayed responses in the machine’s actions.
Cavitation Damage
How does a hydraulic reservoir influence deaeration?
Unfortunately, it’s impossible to completely eliminate air in a hydraulic system, so best way to handle air in your oil is to influence how the air behaves.
Enabling deaeration involves encouraging any bubbles to coalesce and escape the oil. In a hydraulic system, the hydraulic reservoir is where this deaeration happens.
Ideally, any air bubbles that form in the hydraulic fluid will exit the fluid and disperse into the open headspace of the reservoir.
The key to air removal in the reservoir is reducing fluid turbulence in the reservoir.
Fast, turbulent flow in the reservoir keeps air bubbles circulating and suspended in the fluid for longer. In extreme cases, flow may be high enough that it causes surface disruptions that draw more air into the fluid.
A tank assembly that can reduce the turbulence of flow allows air bubbles to coalesce, rise, and escape from the oil more easily. This can be accomplished with thoughtful tank geometry and carefully selected in-tank filtration.
Eliminating turbulence is also critical for keeping air out of suction lines. The longer air bubbles remain in the reservoir before being drawn into the suction lines, the better their chance of coalescing and escaping the oil. Reducing turbulence is a good way to boost air residence time.
One of the ways that conventional reservoir designs have tried to increase air residence time and combat flow turbulence is by simply making the reservoir bigger.
Increased volume can dampen turbulent flow and increase air residence time…but oversized reservoirs come with some major downsides:
Larger reservoirs require more oil, which drives up oil-related costs.
Bigger, heavier reservoirs increase overall equipment weight and reduce energy efficiency.
With a bigger tank assembly, less space is available for design innovations and other useful features.
How can Tank Optimization and Air Fusion Technology filtration improve my reservoir?
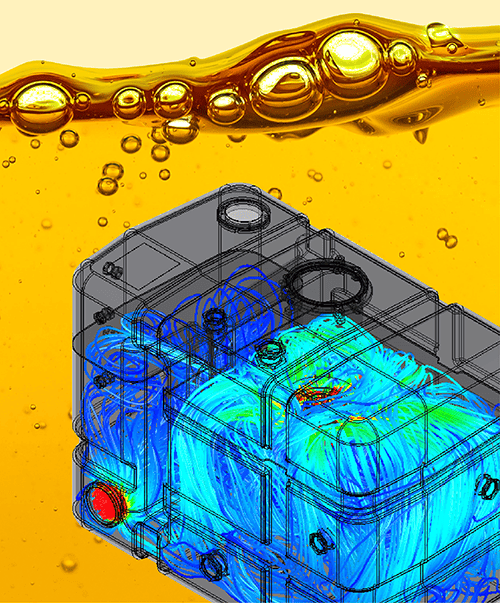
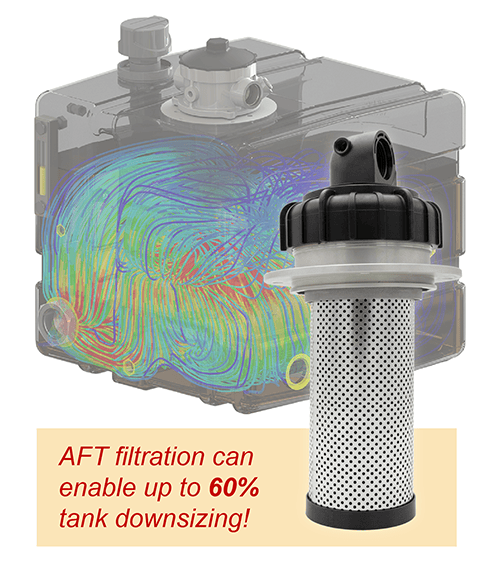
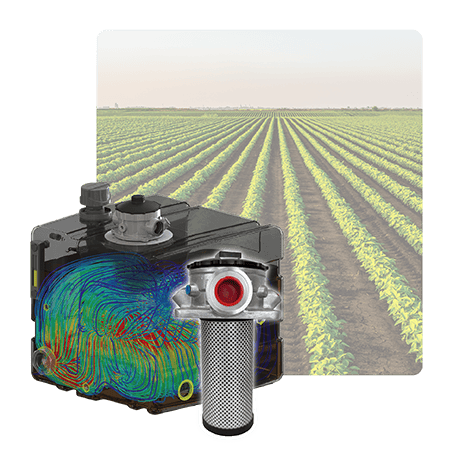
Schroeder Industries’ Tank Optimization uses specialized digital simulations to analyze the existing properties of a tank, identifying inefficiencies in the design. From there, our tank assembly and hydraulic system experts develop a solution that optimizes deaeration and improves overall tank performance.
When paired with purpose-built deaerating filtration, this optimization and redesign process often enables significant reservoir downsizing.
When Tank Optimization meets Air Fusion Technology, reservoir deaeration is maximized.
Tank Optimization analyzes flow, fluid sloshing, structural characteristics, and air residence time—all critical factors in reducing (or potentially worsening) air contamination. Based on the initial analysis, failures of the existing design can be identified and corrected to improve air removal.
See how these real Schroeder Industries clients achieved significant tank assembly downsizing by combining deaerating filters with Tank Optimization:
Tank Optimization + AFT Produces 77.8% Reservoir Reduction
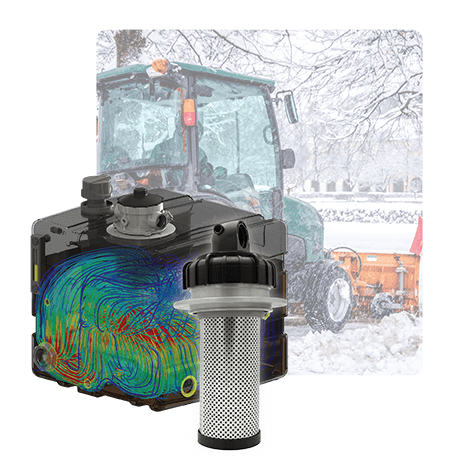
An OEM producing ride-on snow removal equipment, wanting to be more competitive in the market, sought solutions to improve their hydraulic oil cleanliness and optimize their systems.
By combining Tank Optimization with the advanced deaeration of Air Fusion Technology filtration, Schroeder Industries was able to downsize the reservoir from 9 gallons to 2 gallons, allowing the customer to improve their equipment design and become more competitive!
Here’s how Tank Optimization and Air Fusion Technology helped this customer:
Reservoir Downsized by 7 Gallons and 51lbs (77.8%)
Design Improvements: Runs 2x Longer Than Competitor
Tank Optimization + AFT Nearly Halves Reservoir Volume
An OEM manufacturing mobile seed tending equipment sought to assess the performance of their reservoirs and improve their tank design.
This particular customer was producing their own 12-gallon reservoirs in house. Not only could Tank Optimization improve their reservoir design, but any volume reduction would lessen the materials required for manufacturing.
This Tank Optimization, combined with the fixed head Air Fusion Technology configuration (AFTF), was able to downsize the 12 gallon reservoir by almost half.
Here’s how Tank Optimization and Air Fusion Technology helped this customer:
42% Reservoir Downsizing (5 Gallon Reduction)
3,750 Gallons of Oil Saved Across 750 New Units
$40K Reduction in Oil Costs through Tank Optimization
When a buyer is looking for a replacement filter element, the first thing they usually look for is the micron rating of an element. A selection of elements for a given micron rating don’t look obviously different from each other.
So, to cut expenses, buyers may lean towards the lowest cost option.
Here’s why that’s a mistake.
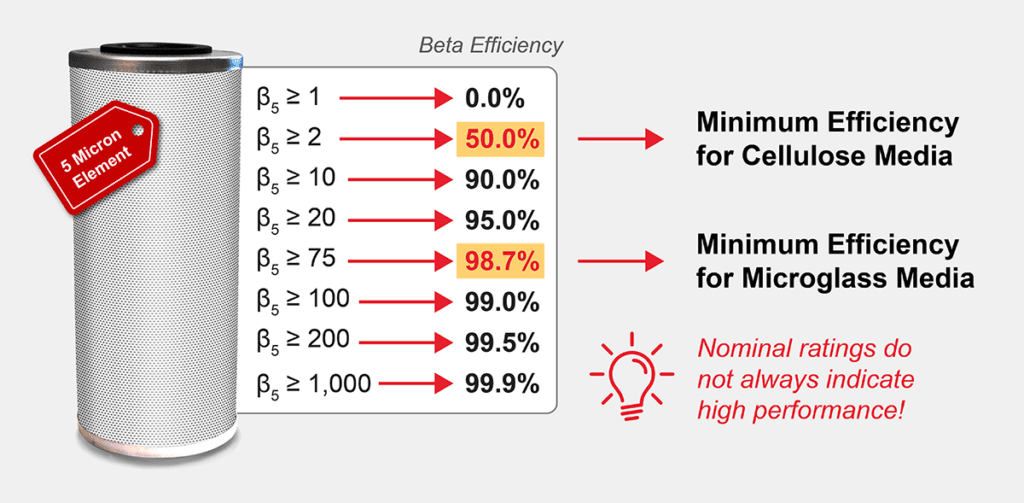
When an element is classified as a 5 micron element, etc, this is known as a nominal rating. To earn a nominal rating, a filter element needs to meet a minimum filtration efficiency requirement for particles of that size.
However, the minimum efficiency can vary greatly depending on the materials used in the filter element! For elements constructed with cellulose media, the minimum efficiency requirement is only 50%.
Microglass media elements need to meet a much higher threshold. An efficiency of 98.7% is required to meet the nominal rating for a given particle size.
Would you trust an element whose efficiency might be as low as 50% to protect your equipment?
Probably not!
But if the nominal rating is not a reliable indicator of performance, what should a buyer look for?
A filter element’s beta efficiency is determined through laboratory testing in a controlled filtration environment.
Let’s compare two elements in an example filtration scenario:
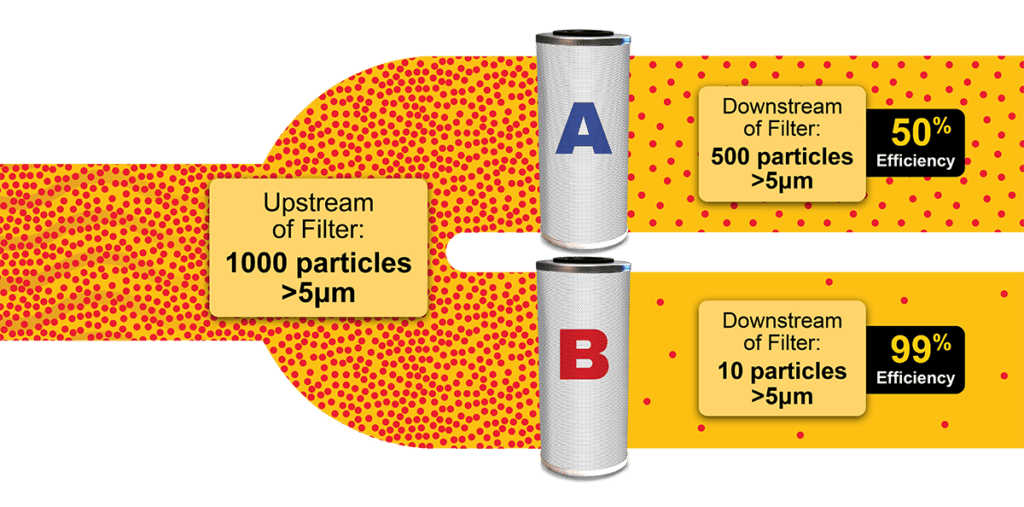
With 1,000 particles 5 microns or larger upstream of the element, we can see how efficiently our two elements capture particulates.
Filter Element A only captures 500/1,000 particles >5µm, which makes its beta efficiency 50% for 5µm. This indicates relatively low efficiency.
Filter Element B, on the other hand, captures 990/1,000 particles >5µm, giving it a beta efficiency of 99% at 5µm. This is considered high efficiency.
In Summary:
Nominal Rating:
Indicates that a filter element meets minimum filtration performance requirements. Should not be treated as a definitive measure of element performance.
Absolute Rating:
A precise measurement of filter element performance, based on beta efficiency. More accurately describes element performance versus a nominal rating.
How do I find the absolute rating of a filter element?
For more information about absolute rating and other performance metrics, try searching for more information on the manufacturer’s website.
Absolute ratings are often expressed in manufacturing literature as beta ratios, which are a kind of shorthand for beta efficiency. Check out the video below to learn how to convert a beta ratio into a percentage!
The filtration experts at Schroeder Industries have delivered filtration success for customers across a wide spectrum of industries. Whatever the scope or focus of your application, our qualified filtration specialists can work with your team to help determine the most effective replacement filter element solution for your application.
Through private labeling and Quality Protection, we also help OEM’s deliver on their brand’s performance promises for end users.
Due to pressure drop and cost-related concerns, end users operating frac trailers were reluctant to adopt higher-performance, smaller micron-rated elements despite their existing 40 micron elements inadequate performance.
To satisfy customer concerns and increase their system protection, Schroeder Industries engineered a new element specifically designed for the types of filter commonly seen in these frac trailer applications.
Head to head testing proved that the new 25 micron Schroeder BestFit element option greatly outshines the customer’s current elements while remaining cost-competitive!
Here’s how Schroeder Industries’ Element Technology helped this customer:
An OEM producing marine dredging equipment was being blamed for premature field failures, and grappling with increased warranty claims.
The culprit behind the failures was actually the substitution of low-quality filter elements by the end users. These elements failed to effectively control contamination, resulting in rapid component degradation and unexpected failures.
To reinforce the OEM’s warranty protection and encourage appropriate element usage, Schroeder Industries partnered with the OEM to establish a private labeled element program.
Here’s how Schroeder Industries’ Element Technology helped this customer:
Posted by McKenzie Thorpe on | Comments Off on Can Better Water Control Protect Your Hydraulic Oil?
Water contamination can sink your productivity and drown your budget.
Solid contamination is the most common type of contaminant, but water contamination can be just as damaging.
Water contamination in hydraulic oil occurs when dissolved, emulsified, or free water enters the fluid and reduces lubrication, promotes corrosion, and accelerates component wear.
The risk is constant in applications that utilize large quantities of water or are exposed to weather and ambient humidity.
Uncontrolled water contamination damages equipment and productivity for any hydraulic system operating in such environments:
Water contamination lowers oil lubricity, which accelerates component wear.
Rusting, corrosion, and oxidation can occur as water interacts with internal system components.
Physical damage such as macro-pitting (spalling) and micro-pitting can occur in cylinders, gears, and other parts.
Ultimately, total machine failures may occur, forcing operations to halt.
Paying to replace oil or hiring a third party oil reclamation service can seriously undermine your profits—not to mention the cost of equipment repairs and lost productivity
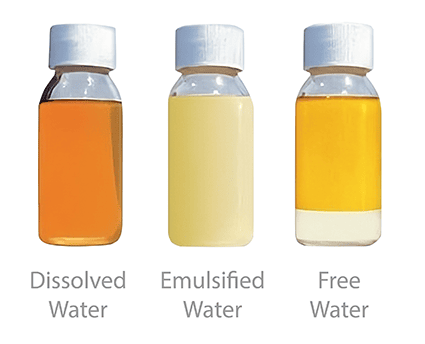
Water contamination comes in three forms, with different levels of severity for your equipment:
Free Water: The worst kind of water contamination. Free water is a separate, visible layer of water that forms when hydraulic oil exceeds 100% saturation.
Emulsified Water: As saturation approaches 100%, small water droplets are visibly suspended in the fluid, giving it a cloudy appearance. While not as inherently damaging as free water, emulsified water is a clear warning sign of contamination approaching a critical level.
Dissolved Water: Considered the least harmful state of water contamination. However, extreme temperature changes can cause dissolved water to separate and become free water.
Changes in temperature can cause water to change form in your system, moving between these three states.
Regardless of how the water in your oil is behaving at one moment, it can go from relatively harmless to increasingly damaging when temperatures start to shift! This means that controlling all water contamination at all times is vital.
Is my operation vulnerable to water contamination?
Virtually any industry can experience some level of water contamination. However, some industries stand out as particularly vulnerable:
Marine: The risk of water contamination when operating on rivers, lakes, and oceans goes without saying! Additionally, swings in temperature in these outdoor environments can cause free water to form, flooding the system with the most damaging state of water.
Pulp & Paper: High volumes of water are required in pulp processing and paper production. In these applications, water contamination is a common pain point.
Steel: High heat applications mixed with high-pressure cleaning spray-downs creates intense humidity. Temperature changes in steel plants can easily trigger condensation of water into the hydraulic reservoirs.
Water contamination can infiltrate reservoirs and equipment in multiple ways.
Damaged seals, a rainy and humid climate, high-pressure water streams used in the cleaning process, and poor bulk oil storage are some common vectors for water contamination. Because water contamination can come from so many places, creating a plan to combat it can be challenging.
How can I prevent water contamination in my hydraulic oil?
Step 1: Test your oil to determine saturation levels.
If you suspect water contamination, it’s important to test your oil. When you know the saturation levels you’re dealing with, it’s easier to develop a strategy for water removal.
Saturation sensors are a great way to detect water contamination in real time. Lab testing is even better, since more sophisticated testing methods can expose other contamination-related problems in your fluid.
Step 2: Examine your equipment and operating environment for vulnerabilities.
Knowledge is power! Finding out where the water contamination is originating from can help prevent it.
Water may be entering via worn seals, loose reservoir caps, poor bulk storage practices, and other variables you can control.
However, many operations may face ambient humidity, big temperature swings, and the unavoidable need for water in their manufacturing process. When a potential source of water contamination can’t be controlled, the best defense is to continuously extract the contamination from your hydraulic oil.
Step 3: Implement water removal filtration tools.
Once you’ve determined how much water you’re dealing with, and where it might be coming from, the next step is filtration. Depending on the amount and frequency of water contamination, there are various tools at your disposal.
Specialized water-removal filter media can absorb smaller quantities of water. Multi-stage filtration housings can allow you to implement different media types to target both water and solid particulate contamination at once.
Large reservoirs and high contamination levels require more specialized equipment. Dehydrating filtration systems are designed to extract free water, as well as a large portion of dissolved water from the fluid.
Step 4: Continuously monitor your fluid condition.
Even with filtration in place, it’s important to implement a strategy for monitoring saturation levels in your oil at all times. Saturation sensors are useful for determining if your dehydrating filtration solution is performing adequately. These sensors can also warn of sudden influxes of water contamination, allowing remedial measures before contamination-driven damage can run rampant.
Many modern saturation sensors include digital connectivity for remote monitoring and reporting, which keeps you informed of your fluid condition in real time, wherever you are.
Schroeder Industries offers a variety of tools and solutions for water removal.
Our Triton Dehydration Stations offer proven performance for oil reclamation in larger reservoirs and high contamination scenarios.
These units are engineered to eliminate 100% of free water and up to 90% of dissolved water by leveraging a patented mass-transfer dehydration technology.
Here’s how Triton Dehydration Stations helped these customers save substantial quantities of oil:
TDS-A Saves Tens of Thousands in Oil-Related Expenses for Injection Molding Equipment
A plastic packaging operations was experiencing high levels of water contamination in their injection molding equipment’s hydraulic reservoir.
The customer was spending tens of thousands of dollars per month on oil recycling costs and new oil purchases.
Schroeder Industries deployed a TDS-A unit to dehydrate their oil, as well as extract any particulate contamination, to ensure operational reliability slash the customer’s oil-related expenses.
Here’s how the TDS-A helped:
16/14/12 ISO Code Reached; Cleaner Than Customer’s ‘New’ Oil
$25-30k USD Saved Per Month on Oil-Related Expenses
220gal of Hydraulic Oil Reclaimed in Just Two Days
TDS-E Saves Pulp & Paper Manufacturer $10K Per Month in Oil-Related Expenses
A manufacturer in the pulp & paper market required additional water removal capacity in their power generation turbine reservoir.
While the operator tried to implement a non-Schroeder dehydration unit, it was unable to keep up with the high volume of water infiltrating the reservoir.
To allow the customer to test the performance of the TDS-E, Schroeder Industries enrolled them in the rental equipment program to prove the unit’s effectiveness.
Here’s how the TDS-E helped:
Rental Program Provides Affordable Access
TDS-E Provides Exceptional Oil Reclamation with Minimal Maintenance
Posted by McKenzie Thorpe on | Comments Off on Roll-Off Cleanliness: The Proven Way to Prevent Equipment Failure
When equipment fails prematurely, contamination is often to blame.
For OEMs, premature failures may mean paying out for a costly warranty claim—and, in some cases, exposure to legal liability. Not only do these failures cost the OEM, but they massively inconvenience the end user, and can undermine the manufacturer’s brand reputation.
To reduce the chances of premature failures, every OEM should uphold a high standard of roll-off cleanliness. Fluid filtration is a key aspect of roll-off cleanliness.
How Fluid Contamination Becomes Built-In Contamination
‘Built-in’ contamination refers to contamination that infiltrates a new machine during the assembly and testing process, prior to final delivery to the end user.
Built-in contamination is commonly caused by contaminated components. Metallic fragments lingering after the machining process, or even ambient dust from poor storage and handling practices, can prematurely sideline a machine.
Dirty hydraulic fluid and diesel fuel used to test and fill a new machine can also deliver damaging contamination into the system!
Modern hydraulic and diesel fuel systems have increasingly stringent cleanliness requirements for fluid.
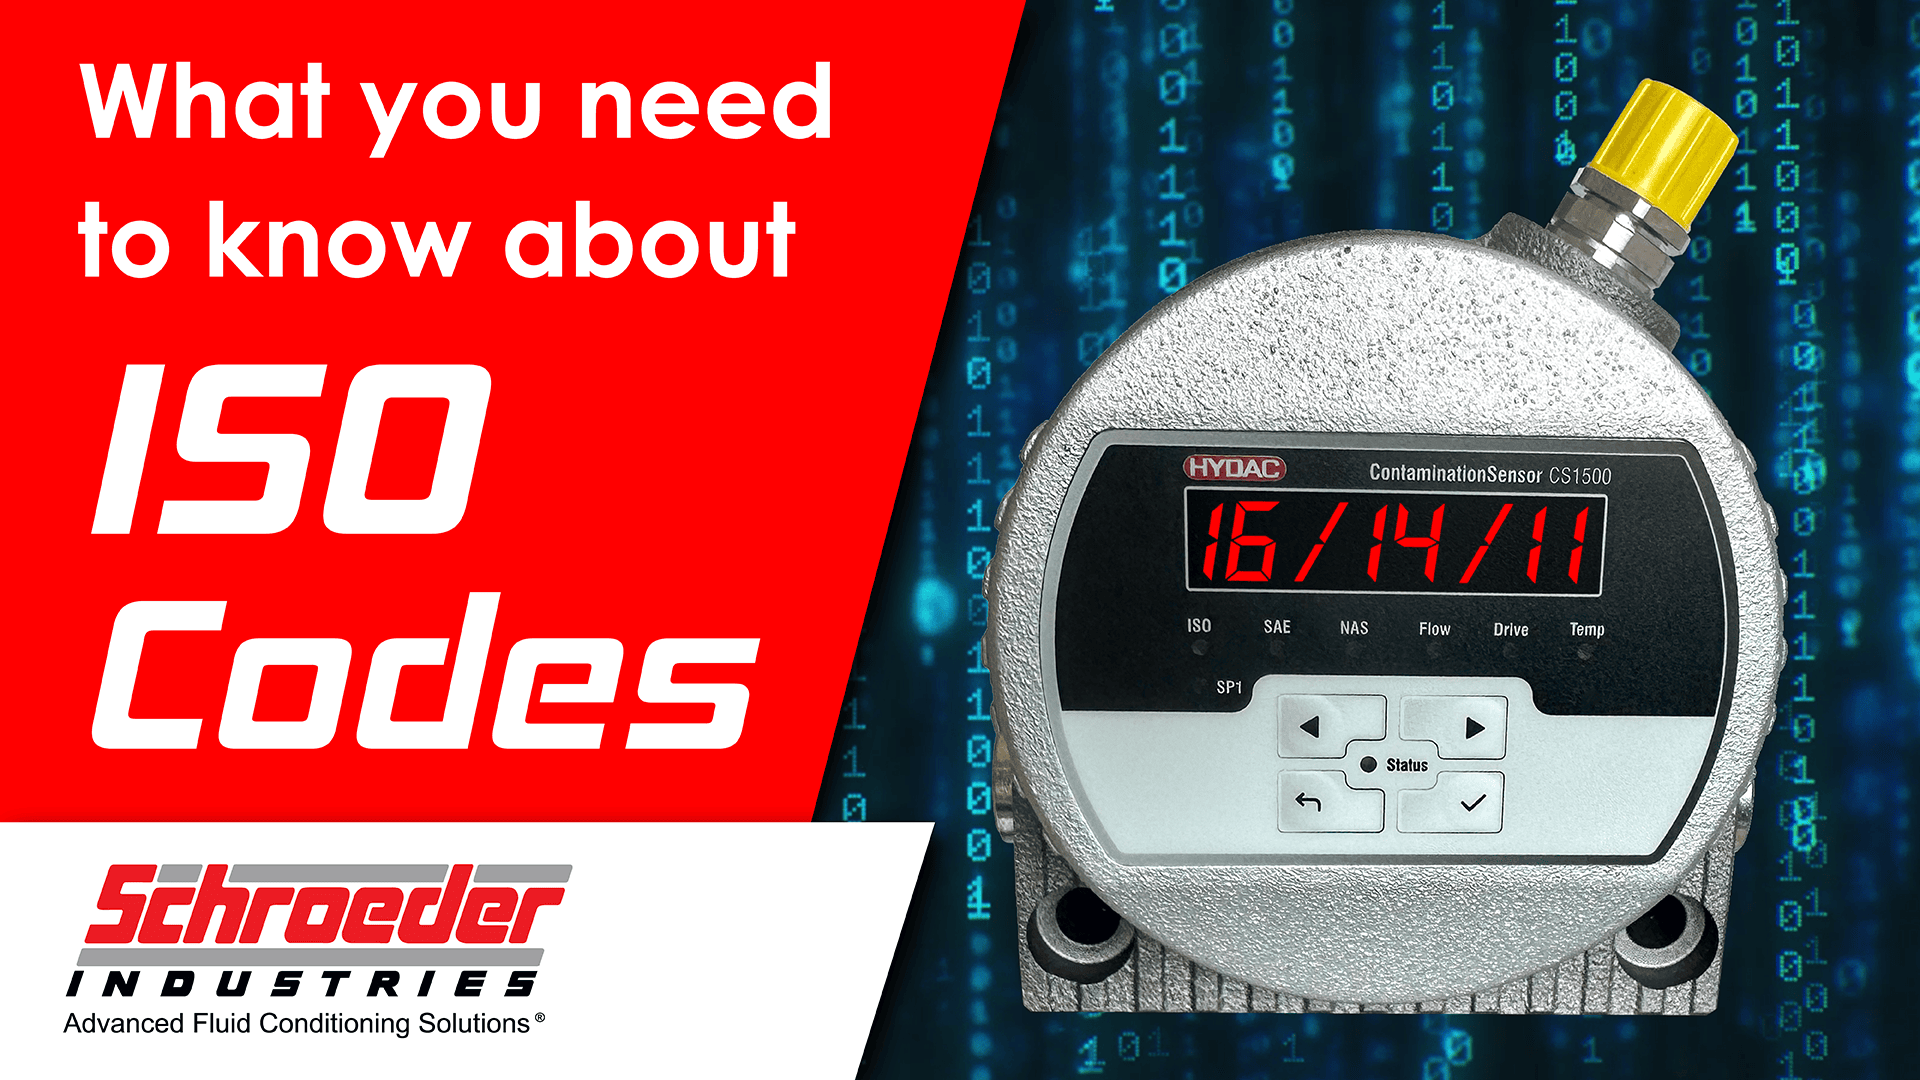
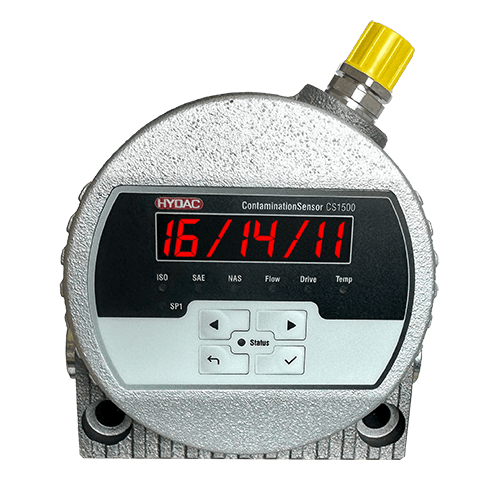
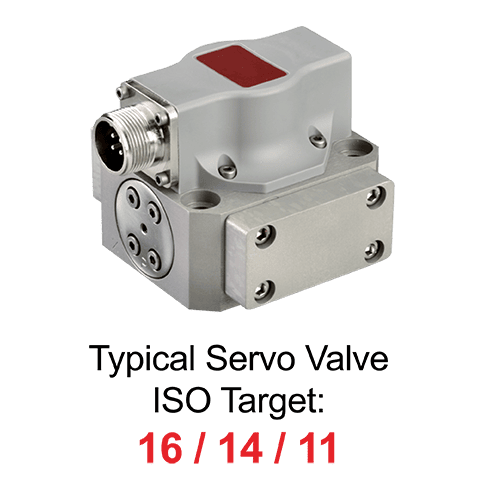
For a modern hydraulic system, the typical standard of cleanliness is an ISO reading of 16/14/11.
Modern Tier IV diesel systems experience higher pressure and contain components with greater sensitivity, so fuel entering the injectors should be less than ISO 12/9/6. That’s 16x more restrictive than the modern hydraulic standard!
You should never assume that your stored fuel or hydraulic fluid is clean, even if it is ‘new!’
‘New’ hydraulic fluid has been found to contain contamination levels as high as 32 times the recommended ISO cleanliness levels for modern systems.
Diesel fuel that has been ‘safely’ stored could be accumulating high levels of water contamination in the background, triggering microbial growth and generating solid contamination within the tank.
If a manufacturer fills the hydraulic and fuel tanks of a machine with contaminated fluid, they are setting the equipment, the end user, and themselves up for failure.
The moment the machine leaves the assembly line with dirty fluid, contaminants begin dealing damage throughout the system.
End users may experience:
Premature Equipment Failure
Impacts to Productivity
Worker Safety Hazards
OEM consequences may include:
Costly Warranty Claims
Legal Liability
Damaged Brand Reputation
To prevent this fluid-borne contamination, any and all operating fluids should be examined and filtered prior to ever touching a machine. As an extra precaution, the equipment’s systems should be flushed and filtered before final delivery as well.
Filtration Solutions for Roll-Off Cleanliness
Schroeder Industries understands the importance of setting end users up for success through roll-off cleanliness. We offer a variety of filtration solutions and diagnostic tools that ensure your equipment is putting its best foot forward from a cleanliness standpoint when it leaves the assembly line.
Diagnostic tools like the TFC are used for establishing ISO counts for fluids in real-time. With particulate shape and size recognition software, the TFC can even provide clues as to where contaminants may be originating from.
Lightweight, hand-held units like the HFS-15 provide the same powerful filtration as a filter cart system with unprecedented mobility. Units with onboard particle counters are available.
Offline filtrations systems such as Schroeder’s array of filter carts (including the MFS, FS, and AMFS) allow for flexibility and mobility. They can act as kidney loop systems for flushing systems, or provide filtration as fluid is transfered into the system.
Ranging from streamlined-but-reliable basic cart systems to advanced systems with onboard particle counting and recording capabilities, these filter carts ensure the cleanliness of fluid within the equipment and can be customized for your specific needs.
Schroeder’s Fuel Filtration division specializes in coalescing and particulate filtration for diesel fuel.
Products like the BDF, GHCF, and more provide superior filtration at every stage of the fuel supply chain, including during transfer, point of fueling, and kidney loop circulating filtration for bulk storage tanks.
Fuel filtration carts like the BDFC combine our world-class fuel filters with integrated pumps, hoses, and a mobile cart chassis.
These turn-key, complete systems offer increased flexibility and enable easy transitions from application to application around a manufacturing plant or storage facility.
The nature of marine environments mean that water contamination is the primary risk to diesel fuel and hydraulic fluid on boats and ships. However, water itself is also a critical operating fluid for many vessels, especially large ships.
In this post, we’re focusing on the role of ballast water in ship operation, and the associated contamination risks.
Ballast Water Contamination
Ballast systems are crucial for the operation of large vessels.
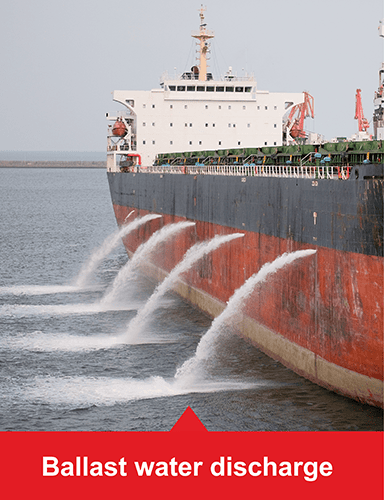
To maintain stability and adjust draft (the height of a vessel in the water), large quantities of water are drawn in from around the ship into tanks within the hull to serve as ballast, and expelled as needed.
Ballast water levels are often increased and reduced multiple times during a voyage to accommodate for cargo movement and obstacles such as bridges. During severe weather, ballast is typically increased to lower a vessel’s center of gravity and reduce the surface area exposed to high winds and waves.
If ballast systems operate inefficiently or fail, consequences including capsizing or collision with structures may occur.
When contamination infiltrates a ballast system, the consequences are far-reaching:
Component Wear & Damage
Sand, silt, shells, and other solid particulates drawn in to the ballast tanks will damage pumps and other critical system components, forcing repairs or causing failures. Malfunction of the ballast system, which is key to vessel stability, is extremely hazardous.
Invasive Species Proliferation
When ballast water is drawn from the surrounding environment, living organisms can be pulled into the ballast tanks and later expelled in an entirely new location where they are not native. This has proven, devastating consequences for marine ecosystems.
Ballast contamination goes beyond just vessel safety and efficiency.
Failure to meet these standards can result in civil fines, criminal penalties, and even denial of entry to port.
Ballast water contamination is responsible for environmental disasters such as the quagga and zebra mussel infestations in the Great Lakes and other North American waterways. These invasive mussels have serious, negative impacts on freshwater ecosystems and industrial operations that rely on natural water sources.
Powerful Process Filtration Eliminates Ballast Contamination
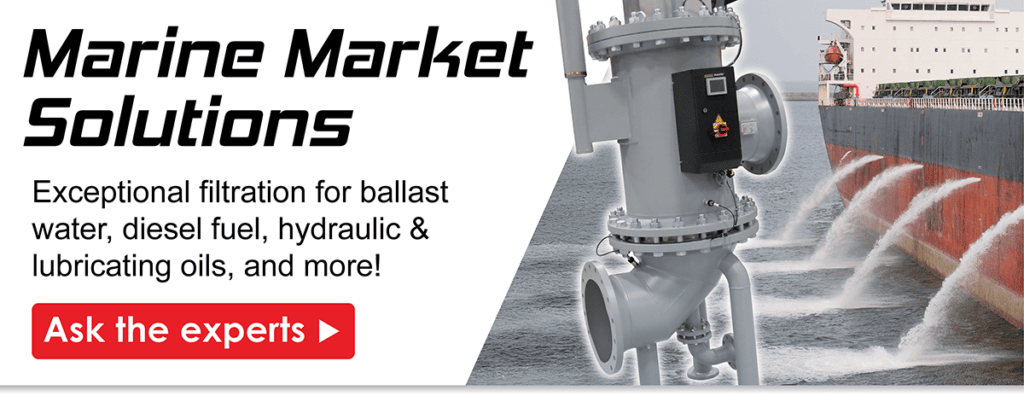
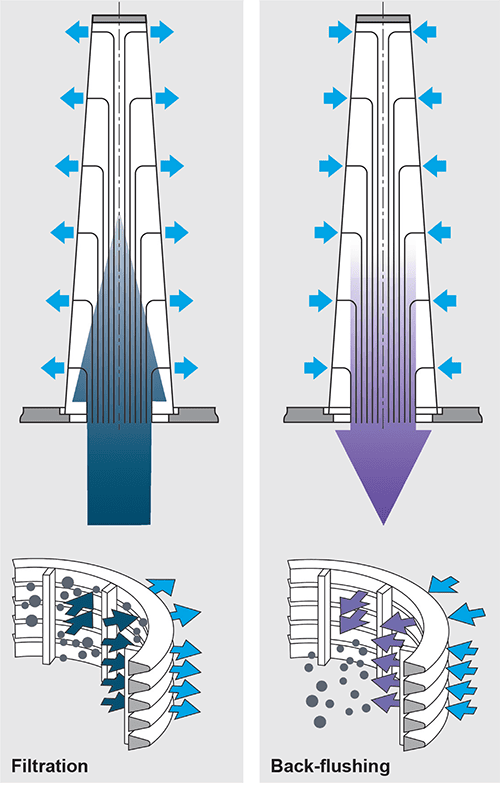
Automatic back-washing filtration excels at contamination removal.
To handle the huge quantities of water that pass through ballast systems, high-volume filtration is crucial.
The AutoFilt® series offers proven performance in the removal of solid contaminants while being maintenance-friendly and efficient.
The self-cleaning, automatic back-flushing system in each AutoFilt® system clears the elements with virtually no interruption to filtration functionality. This automated cleaning function ensures reliability and reduces maintenance, allowing vessel operators to focus their energy on other critical tasks.
Additionally, when paired with disinfectants that target organisms in the ballast water stream, these filters allow operators to meet the IMO and USCG regulations that focus on invasive species containment. Peace of mind and protection from fines and operational delays contribute to smooth sailing!
Our experts in filtration systems can help you select and integrate the right solution for your application.
Meet two of their favorite picks for ballast water contamination control:
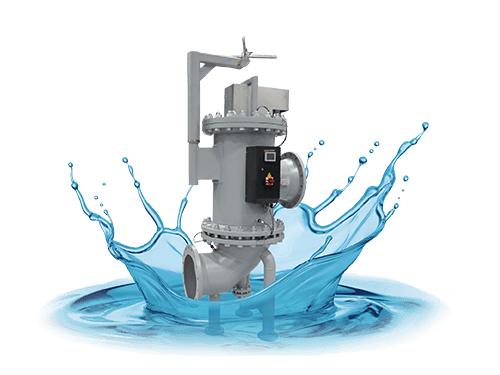
AutoFilt® RF3
395-1120 gpm (420-1800 L/min)
Automatic back-flushing filter ideal for hard particulates like rust and sand. Use in conjunction with disinfection to meet IMO/USCG regulations for ballast water
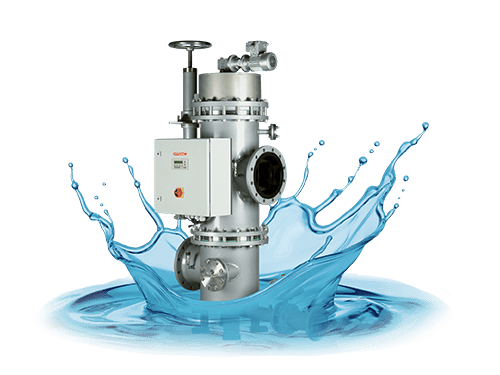
AutoFilt® RF10
2,210-12,940 gpm (580-3420 L/min)
Continuous filtration even during back-flushing. Use in conjunction with disinfection to meet IMO/USCG regulations for ballast water.
Comprehensive Filtration Solutions for Marine Applications
Schroeder’s solutions go far beyond just ballast water filtration!
Here are just two of our other proven solutions for contamination control in marine applications:
Hydraulic Fluid Dehydrators
TDSE, TDSA
Critical vessel systems like bow thrusters, hatch covers, and stabilizers rely on clean hydraulic fluids. In such a water-filled environment, powerful dehydrating filtration is essential for hydraulic system function and longevity!
Learn More
Bulk Diesel Filters
BDFP & More
Engine failure due to fuel contamination is one of the greatest risks in a marine environment! Solutions like Schroeder’s BDFP tackles the threat on two fronts, extracting solid particulates and eliminating water contamination.
Learn More
More Marine Filtration Solutions
Ask the Experts!
Our team is happy to assist with your filtration needs for ballast water and more. Tell us about your application, and we’ll tell you how we can help!
Posted by McKenzie Thorpe on | Comments Off on Data Center Filtration: The Proven Way to Protect Uptime
Data centers impact our lives more than we realize.
Currently, the buzz regarding data centers focuses on the artificial intelligence boom, but these operations are already quite integrated in our day-to-day.
Data centers range from simple server rooms managed by individual enterprises to massive, standalone operations. At their core, the function of every data center is similar: Storing data and applications, and enabling people to access data and web-based services.
Data center outages can result in significant financial losses, service disruptions, and reputational damage, making uptime and infrastructure reliability critical considerations for facility operators.
Apps, websites, and other internet-based resources we rely on may become inaccessible. Because much of the economic and social fabric of society now relies on internet connectivity, these outages range from inconvenient to downright costly!
Even a relatively small data center can be vulnerable to overheating, power outages, and other issues that trigger downtime.
As data centers grow larger and more numerous, and the stakes for failure get higher, preventing outages becomes even more crucial.
How Contamination Causes Critical Failures
Contamination is a hidden threat that compromises equipment across virtually every industry, from hydraulic construction equipment, to diesel-powered ships, to hydro-power systems, and much more. When it infiltrates operating fluids (lubricating oils, liquid fuels, process fluids, etc), trouble is on the horizon for affected equipment.
Contamination can be solid particles, such as tiny metal fragments caused by wear, or dust particles ingested into reservoirs, process water streams, and storage tanks. These particles of solid contamination are often smaller than the eye can see, but even microscopic particles cause wear and tear that eventually lowers the efficiency of the equipment or causes it to fail.
Contamination also commonly presents as water, such as rainwater or humidity that condenses inside of storage tanks. This can reduce lubricity and encourage microbial growth in diesel fuel, and ultimately contributes to equipment failures in a myriad of ways.
Contamination affects virtually every industrial operation—data centers are no exception.
In data centers, there are two key areas that require vigilant defense from contaminants:
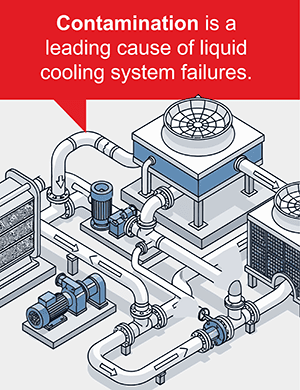
1. Contamination and Liquid Cooling Systems
Thermal management is one of the biggest challenges facing data centers.
The processing power packed into data centers generates an enormous amount of heat. Liquid cooling systems are the preferred choice for thermal management, especially in larger data centers.
However, like any fluid-powered system, cooling loops are vulnerable to contamination.
‘Built-In Contamination’: A freshly constructed cooling system might not sound like a place where contamination would be abundant. However, solid particles left over machining processes, dust and grit that entered during construction, weld spatter, and more can be waiting in the cooling system before the first server even powers on.
Water Source Contamination: Cooling loops can draw from a variety of water sources, including ‘gray’ (non-potable) water and even natural surface water sources such as rivers and lakes. These sources may contain contamination ranging from large visible solids to microscopic particles, all of which can damage the cooling system. Even municipal tap water can contain minerals and sediment that contribute to component wear.
Inevitable Wear & Tear: As components within the cooling system are degraded over time, they can release solid particulate into the system which accelerates the wear process.
What happens if cooling systems fail due to contamination?
To ensure proper performance, it’s important for servers and computing systems to stay as cool as possible.
Overheating can damage servers and computing components, resulting in data losses, major service interruptions, and astronomical repair costs.
2. Contamination and Backup Power Generators
Mission-critical backup power is essential for continuous, 24/7 data center uptime.
In the event of an emergency that affects a data center’s primary power source, backup generators are a critical safety net to ensure that the servers stay running. Diesel-powered generators are the most common choice for reliable backup power.
However, diesel generators can be especially vulnerable to contamination. Because these generators sit idle for long periods, it’s easy for contamination-related problems to be overlooked until the generators fail when they’re needed most!
Stored Fuel Contamination: Fuel storage tanks can be exposed to environmental contamination in the form of rain, ambient humidity, dust, pollen, and more. If the stored fuel is not regularly tested and filtered, contaminants can build up to critical levels.
Diesel Bug: When water contamination is present in stored diesel, microbial growth known as ‘diesel bug’ will grow along the border of the diesel and free water, essentially feeding on the energy in the fuel. If left unchecked, thick microbial mats can proliferate throughout the fuel, and can quickly foul filters and damage engine components when the fuel is drawn from storage.
Engine Failure: Large quantities of contamination in stored fuel can overwhelm the engine, causing startup delays or even complete engine failure. This not only leads to costly downtime in a data center setting, but may require expensive repairs.
What happens if backup power generators fail?
Even a temporary loss of power can cause chaos and delays for any operation relying on a data center to store data, access critical applications, and more.
If the primary power source fails and backup generators aren’t able to close the gap, power outages will disrupt services, result in SLA violations, and drive significant financial and reputational losses.
Your Partner for System Reliability
Don’t wait for contamination to impact your data centers: Implement solutions early!
Schroeder Industries is the expert in all things filtration, including for process fluid and diesel fuel.
Our product experts have designed solutions that effectively tackle contamination, protect equipment, and maintain productive uptime in virtually every industry that relies on fluid power.
Whether you’re planning your data center or retrofitting an existing operation with filtration, our experts are here to help.
Posted by McKenzie Thorpe on | Comments Off on Invasive Mussel Control for Process Water Systems
When invasive species appear, ecosystems aren’t the only thing that suffers.
Invasive mussel control is becoming increasingly important for industrial facilities that rely on rivers, lakes, and other surface water sources for process operations.
An invasive species is a non-native organism (plant, animal, etc) that is introduced to an environment where it does not naturally occur, and negatively impacts that environment through proliferating and out-competing native lifeforms.
One infamous plant, kudzu, is a prime example of an invasive species. Originally brough from Asia in the 1800’s for erosion control and other uses, kudzu is commonly referred to as the vine that ‘ate’ the southern United States by escaping cultivation and overwhelming native plant species. Today, large swaths of southern forests are carpeted with kudzu, reduced to a shadow of the diverse ecosystems that existed before the vines were introduced.
Another equally impactful invasive organism is lurking in North American rivers and lakes, with huge ramifications for industries that rely on those waterways.
Invasive Mussel Impacts
While mussels may seem small and inconsequential individually, they spread quickly and colonize waterways in large numbers.
Not only are there huge ecological consequences when invasive mussels appear, but there are significant impacts to industrial operations that rely on mussel-infested water sources.
Ecological Impacts Include:
Invasive mussels out-compete native species and consume large amounts of phytoplankton, which larval fish rely on.
Native fish and shellfish populations can collapse, upending the local ecosystem.
Applications that draw from natural water sources can become contaminated by invasive mussels.
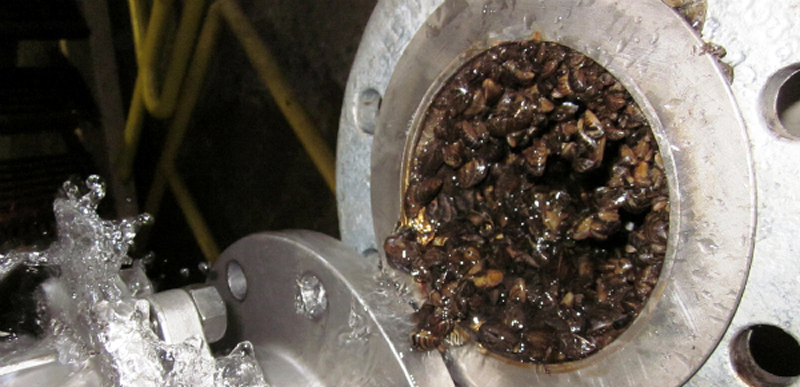
As mussel colonies grow, they can restrict or even block flow entirely.
Chemical treatments, downtime for manual cleaning, unexpected outages, and other operation impacts can cost hundreds of thousands of dollars annually.
All across North America, freshwater ecosystems and industrial processes that rely on natural or surface water sources are under attack.
A Trans-Continental Problem
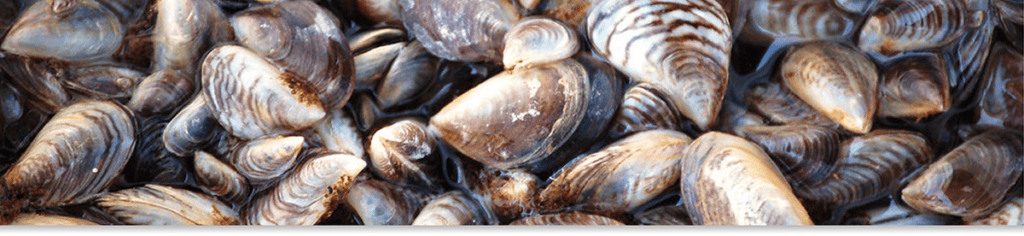
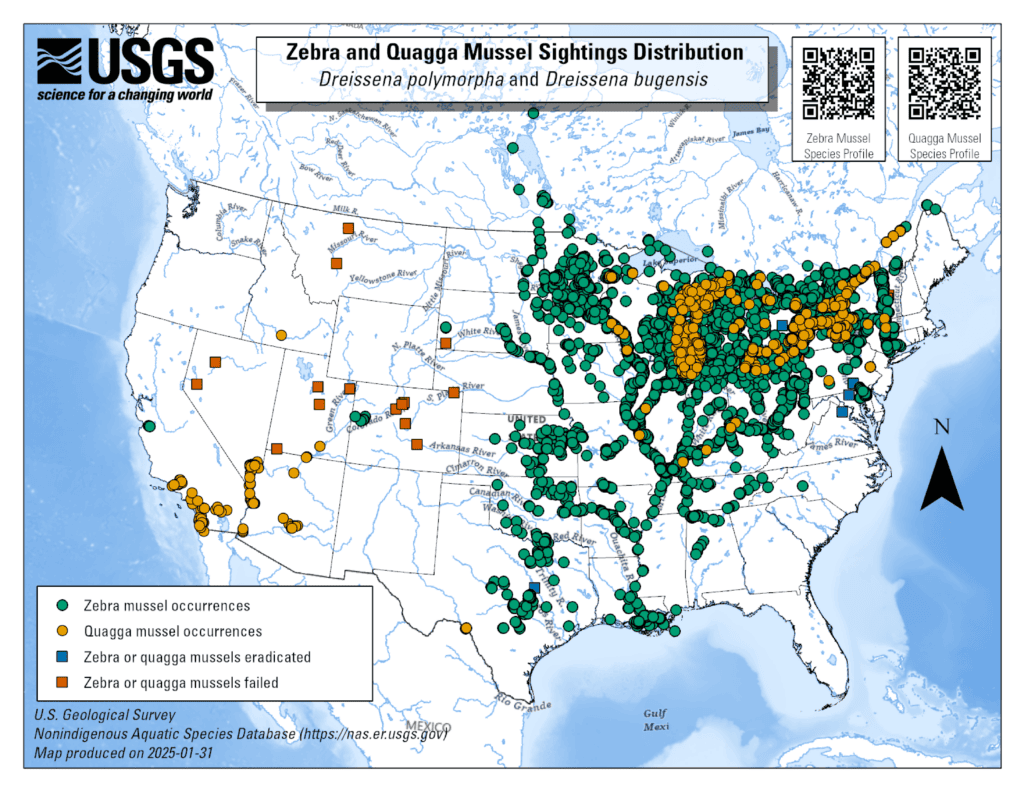
Two specific invasive mussel species—zebra mussels and quagga mussels—have become widely distributed in the Great Lakes and other critical waterways across North America. Once the mussels have infested an area, eradication is virtually impossible.
For operations that rely on infested waterways for process fluids, they are at direct risk of exposure to invasive mussels.
Golden mussels have the potential to be even more damaging than the quagga and zebra mussels.
Because golden mussels can tolerate a wider range of salinity and water temperatures, it opens up new angles of attack on North American water systems.
Additionally, golden mussels seem to breed and spread more aggressively than the other invasive mussel species.
What can be done to prevent golden mussels and other invasive species from infiltrating and damaging critical water infrastructure?
The Cons of Conventional Mussel Control
As long as invasive mussels have been a problem, operations relying on water from lakes, rivers, and other natural sources have tried to combat them. However, the existing strategies for mussel control come with significant downsides:
Conventional screen filtration is effective at catching mussel shells and mature mussels, but mussel larvae can easily squeeze through and begin growing deeper in the water system.
Chemical treatments kill adult mussels and mussel larvae, but leave behind shells and biological debris which must be cleaned out of the system.
Manual removal is purely reactive, and may require extended downtime (and significant disruptions to productivity) to complete.
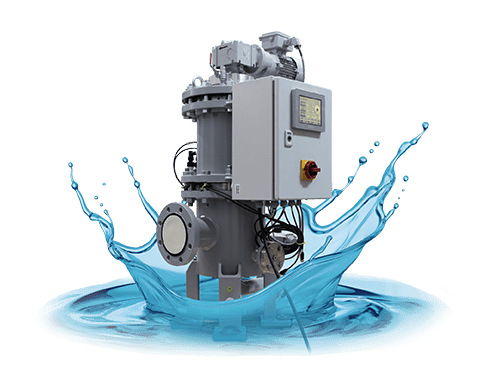
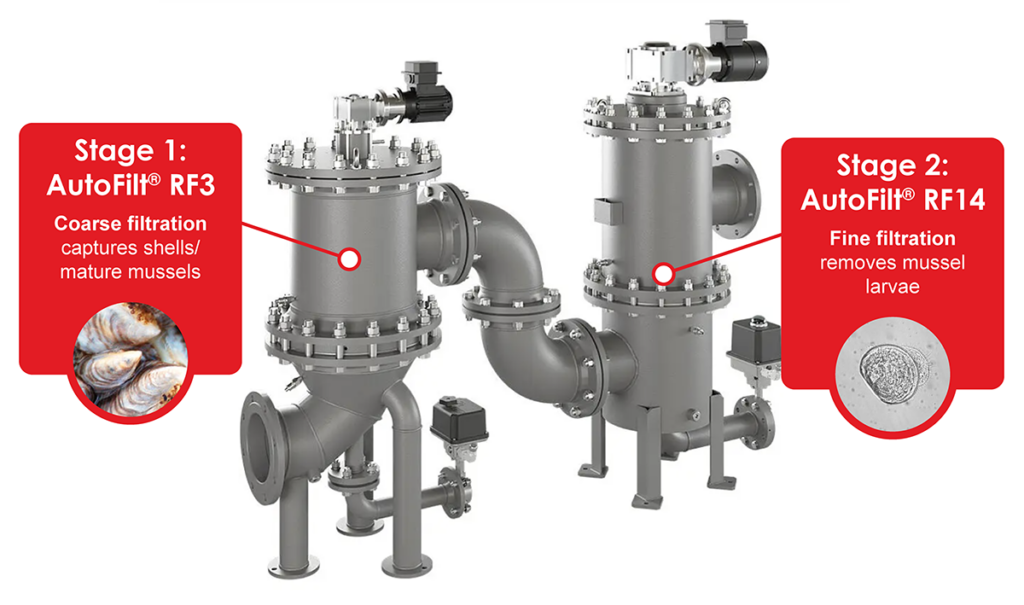
This dual-stage configuration combines two powerful AutoFilt® units that tackle invading mussels in every life stage:
Mussel-Catch Stage 1: AutoFilt® RF3
Highly Efficient Coarse Filtration
The RF3 effectively stops larger solids and shells in their tracks, keeping mature mussels from entering the system and colonizing the water infrastructure.
The automatic back-flushing technology of the AutoFilt® series enables filtration with minimal interruption, clearing the filter elements of solids and maintaining filter efficiency while reducing downtime.
Ask The Experts!
Our Process Filtration division can help you implement solutions that protect your systems from invasive mussels and other common process fluid contaminants. Tell us about your application:
Posted by McKenzie Thorpe on | Comments Off on How to Set ISO Cleanliness Targets for Hydraulic Systems
When it comes to contamination, what you don’t know could be costing you.
In hydraulic systems, up to 70%-90% of wear and failure is contamination related!
To keep your equipment functioning properly, slash repair costs, and operate as efficiently as possible, contamination control is essential. The effects of contamination costs tens of thousands, even hundreds of thousands of dollars for industrial operations across the world every day!
Every person dealing with hydraulic equipment, diesel-powered equipment, and even compressed gases should know some contamination basics.
Let’s review solid contamination, ISO Codes, and ISO Targets, some of the most fundamental principles of contamination control.
Recap: Solid Contamination
Identifying contamination sources is only part of protecting hydraulic equipment. Selecting the appropriate filtration media is also essential for maintaining fluid cleanliness. Schroeder offers a range of hydraulic filter elements designed to support contamination control across industrial applications.
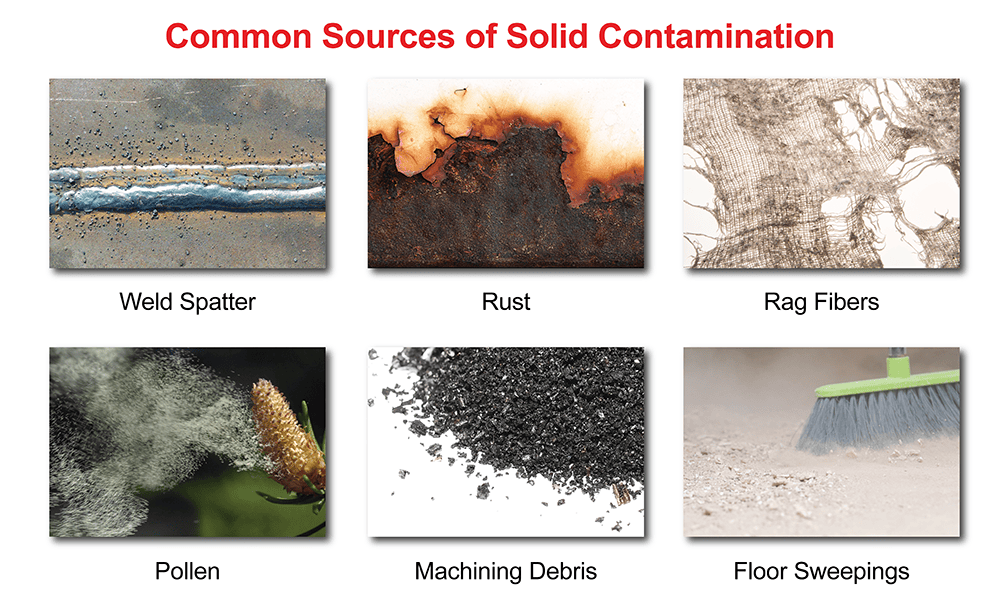
Solid contamination is the most common, and often the most destructive form of contamination in fluid-powered systems. There are countless opportunities for solid contamination to infiltrate hydraulic fluid, diesel fuel, and other operating fluids:
Dust, grit, sand, and other solid particles in the operating environment.
Organic solids such as pollen and debris from trees and other vegetation.
Introduction of ‘new’ fluid that is not adequately filtered. (Never assume that ‘new’ oil or fuel is ‘clean’!)
Machining debris left over from equipment manufacturing and assembly. (This is often called ‘built-in contamination’.)
Solid contaminants are often smaller than the eye can see, but these tiny particles can add up to huge losses in efficiency, productivity, and profit!
In the world of fluid power, solid contaminants are measured in microns, often represented by the symbol ‘µm’. Microns are used to measure particles on the microscopic level.
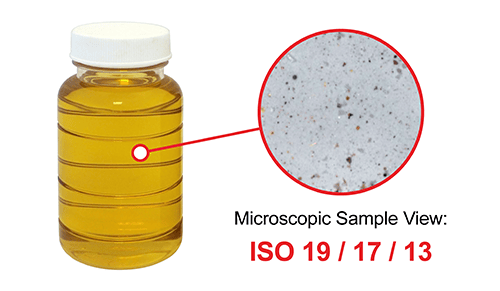
Hydraulic oil or diesel fuel may look perfectly clean to the naked eye. However, a closer look under the microscope reveals a hidden threat: solid contamination. These particles may be microscopic, but the damage they cause to your equipment can be massive!
As microscopic particles of solid contamination grind through your system, they gradually wear down critical components like servo valves, pumps, cylinders, injectors, seals, and more.
When these components eventually fail, the repercussions can range from inconvenient, to costly, to catastrophic for productivity and even worker safety!
Knowing how how to measure solid contamination—and how much contamination your system can handle before risking premature failure—is incredibly important.
ISO Codes: Decoding Solid Contamination
The amount of solid contamination in a fluid system or a fluid sample is represented by an ISO Code.
ISO Codes (pronounced ‘eye-so codes’) are numerical codes used to quantify the amount of solid contamination in hydraulic fluid, diesel fuel, process fluid—essentially, any operational fluid!
ISO Codes consist of three numbers, separated by forward slashes. These three numbers represent the amount of solid particles across three different size ranges in the fluid.
Higher numbers in an ISO Code mean more contamination in the fluid!
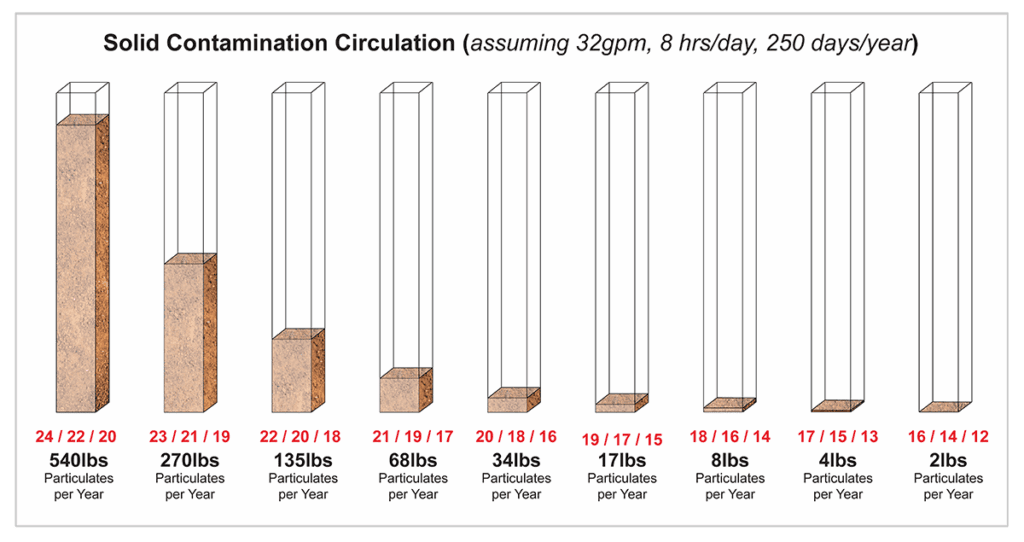
Additionally, with each increase in ISO Class, the amount of contamination is actually doubled. So, if your hydraulic system starts at ISO 16 / 14 / 11, and goes up to ISO 17 / 15 / 12, there istwice as much solid contamination grinding through your system every time you turn it on!
This means that what may seem like a small change in your ISO Code can have huge impacts. Just a few rungs up or down the ISO Class ladder can mean the difference between tens or even hundreds of pounds of solid contamination circulating in your system every year!
If your machine is operating with dirty fluid, this could take years off its life in terms of peak performance. This is why knowing and meeting your machine’s cleanliness targets, also called ISO Targets, is so important!
Tolerances and ISO Targets
ISO Codes are also used to represent part tolerances.
‘Tolerance’ refers to how much contamination a machine component can tolerate and still maintain a ‘normal’ lifespan according to manufacturer guidelines.
Components that are more complex, more sensitive, or located in higher-pressure regions of the fluid circuit, etc. will generally be less tolerant to contamination.
Because tolerance is represented by an ISO Code, an individual component or system’s tolerance is commonly called an ISO Target.
An ISO Target is basically the ISO Code you should aim for in your operating fluid to help your equipment live up to its potential!
Different components within a system may have different tolerances, and thus, different ISO Targets!
The ISO Target for an entire machine or system is based on the component with the lowest tolerance. That way, protection is ensured across the whole system for even the most sensitive component!
How Can I Find My Machine’s ISO Target?
Manufacturer guidelines generally include a minimum ISO Target.
However, a custom assessment could find a target that helps your equipment outlive its expected operational life!
A manufacturer may set a machine’s ISO Target based on a ‘normal’ lifespan for different components.
But, if you can push your fluid cleanliness beyond the manufacturer’s minimum recommendation, it may add years of efficient performance to your machine’s life!
Understanding your equipment’s current fluid condition is the first step toward establishing effective ISO cleanliness targets. Schroeder’s Fluid Analysis Program provides laboratory testing and condition monitoring to help identify contamination, track fluid health, and support informed maintenance decisions.
Want to find out if your equipment could go above and beyond its normal operating life?
Talk to the experts at Schroeder Industries! We can provide a comprehensive analysis of your current ISO Targets and contamination control program, and make customized recommendations that help your equipment live up to its full potential.
Tell us about your applications, your equipment, and your operational goals. We’re here to help!
Introducing a Waste-Eliminating Spin On Filter Alternative
>90%
reduction in wasted scrap metal
>80%
less hydraulic oil waste
>80%
reduction in CO2 emissions
Spin on hydraulic filters are a popular filtration option. These filters combine the filter housing and element as one complete unit, which can be quickly and easily screwed on and off the hydraulic system.
However, the disposable housing also greatly increases the overall cost per change-out. Additionally, there is massive material waste, as the filter housing is thrown away with the element when a spin on filter is replaced.
Enter the Sustainable Cartridge Bowl filter, or SCB!
This revolutionary filter offers the same spin on convenience, with a reusable housing bowl design. The innovative SCB offers a range of advantages:
More cost-effective element replacement compared to conventional spin-on filters
Cuts down on waste and emissions, including a >90% reduction in scrap metal waste
Discards less oil with each change-out, conserving resources
Powered by filter elements with higher pleat counts and lower pressure drop for superior filtration performance
The SCB’s Signature, Patented Innovation
The material and cost savings of the SCB are made possible through its reusable housing bowl.
The secure sealing and glass-infused, injection-molded nylon bowl provide a durable housing for the high-performance element within.
Robust outer bowl provides re-usability and durability.
The outer portion of the bowl is injection molded plastic, supported by an internal steel tube and flange structure. This results in a lightweight, yet durable housing bowl.
The end-cap of the filter element slides over the bowl, forming a seal along the outer rim and preventing operation without a filter element in place.
Coreless filter element design: higher performance, reduced waste.
The coreless filter element design with plastic caps makes disposal simpler. With support from epoxy-coated wire mesh, pleat stability, efficiency, and dirt holding capacity are increased. These premium filter elements also feature a higher pleat count and lower pressure drop, further improving their performance.
How Does the SCB’s Sustainability Compare to Conventional Spin-Ons
Traditional spin on filters contribute to waste and CO2 emissions in two primary ways: wastedscrap metal, and wasted oil.
This waste takes up landfill space and contributes to emissions released during production.
The SCB filter elements, however, are almost entirely plastic and can be easily crushed for efficient disposal. Between these elements and the reusable housing bowl, scrap metal waste is reduced by ~99%.
Extra oil may become trapped in a typical spin on housing, but the SCB only loses oil which has saturated the filter element.
Waste Reduction Example, per 1,000 spin ons:
M10 (cellulose 10 micron) Spin On
1,966 pounds metal scrap waste
If not properly drained, wastes approximately 450 gallons of oil
CO2 emissions: approximately 10,600lbs of CO2
SCB Coreless Replacement Design
Only 20 pounds of metal scrap waste (epoxy wire)
Total oil volume lost through cartridge change-outs: 57.2 gallons (87% reduction versus conventional spin-on filter)
CO2 emissions: approximately 1,300lbs of CO2 (88% reduction versus conventional spin-on filter)
The signature reusable housing bowl of the SCB isn’t just eco-smart: it’s far more cost effective than typical spin on filters.
With a reusable housing bowl, only the filter element must be replaced, which results in exponential savings after just a few element change-outs. And, with the SCB, the first kit comes with a spare element, meaning the first change-out is already paid for.
Over the lifetime of a given piece of equipment, savings can be substantial!
Contact Schroeder Industries or a verified Schroeder distributor for pricing details.
Increased Revenue in Spare Element ROI Strategy
The average aftermarket filter element retention for OEMs is just ~35%.
However, the Quality Protection built in to every SCB bowl and element prevents the use of subpar third-party elements. Not only does this help the end user protect their vital equipment, it can boost aftermarket retention for OEMs to as high as 100%.
Assuming 1,000 machines are produced per year, with 4 element changes per year, substantial gains in aftermarket revenue are possible through a spare element sales strategy:
For increased aftermarket retention, the SCB also includes private labeling options for the bowl and filter elements. To learn more about Schroeder Industries’ private labeling capabilities, view the Private Labeling Capabilities Form.
Petroleum-Based Fluids:Z-Media® and Anti-Static media (synthetic)High Water Content:All Z-Media® and Anti-Static media (synthetic)Invert Emulsions:10 and 25μ Z-Media® and 10μ Anti-Static media (synthetic)Water Glycols:3, 5, 10 and 25μ Z-Media® and all Anti-Static media (synthetic)
SCB Fluid Compatibility
Flow Rating:50 gpm (190 L/min)Max. Operating Pressure:150 psi (10 bar)Burst Pressure:600+ psi (41.4+ bar)Temperature Range:-20°F to 225°F (-29°C to 107°C)up 250°F (121°C) with VitonReplacement Element Case:6 elements
Posted by McKenzie Thorpe on | Comments Off on Ultimate Chill: The Proven Filter Tank Cooler Unit
Overheating is a common, constant issue for hydraulic equipment, especially when working in scorching summer conditions. Over time, this can have negative consequences for critical machinery:
Overheating accelerates oil degradation, causing varnish and sludge to coalesce in the system and cause blockages and reduce operating efficiency.
Shortened oil lifespan forces more frequent oil change-outs, increasing both downtime and oil-related expenses for new purchases and recycling.
Oil degradation products can damage system components and force the equipment’s engine to overcompensate.
Keep Cool and Collected with the FTC
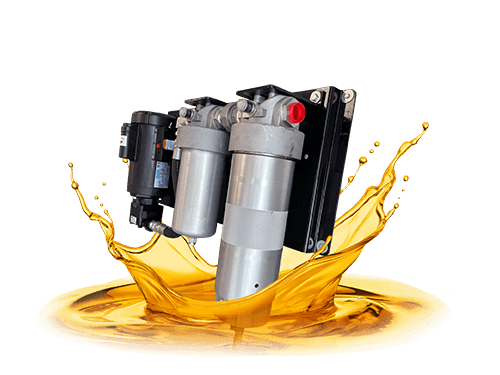
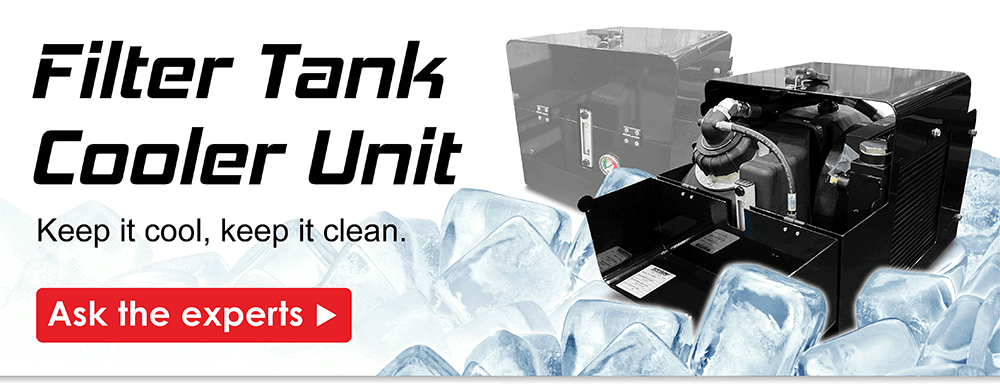
Schroeder’s new Filter Tank Cooling Unit (FTC) is a compact solution for mobile fleet vehicles that combines a hydraulic tank assembly and cooling unit in one complete package.
Condensed, efficient footprint ideal for the space limitations of mobile vehicles; most optimized tank/cooler combination currently available
Integrated cooling unit maintains safe operating temperature, extending fluid life and preventing overheating in the hydraulic system
Reduces weight, space utilization, and oil usage; provides associated cost savings
Air Fusion Technology filtration and a robust, rotomolded 7-gallon TNK design to reduce weight and increase the efficiency of the reservoir’s performance and deaeration capabilities
Schroeder Success: FTC Unit Increases Machine Space on Mobile Fleet Vehicles
An OEM producing mobile fleet units sought a lighter, more space-efficient alternative for their 25 gallon hydraulic unit and separate cooling unit, which took up considerable room on the mobile unit.
Schroeder Industries engineered the FTC unit to utilize space as efficiently as possible while delivering optimal performance from the hydraulic reservoir and cooling unit, allowing OEMs to further streamline and improve their equipment designs.
Here’s how this customer benefited!
Tank + Cooling Assembly Footprint Substantially Downsized
18 Gallon Reduction in Reservoir Size; Reduced Oil Usage Per Unit
Increased Machine Space for Further Design Improvements
Can the FTC Unit help you beat the heat? Ask the experts!
The product experts at Schroeder Industries can help you find the optimal solution for your application. Let us know how we can help!