Posted by McKenzie Thorpe on | Comments Off on How Do Hydraulic Tanks Eliminate Air Contamination?
Your reservoir is more than just a holding space for hydraulic fluid.
“If the reservoir isn’t leaking, all is well, right?”
Actually, the hydraulic tank assembly plays a critical role in removing damaging air contamination from your fluid!
Despite being the central pillar of controlling air contamination, many reservoirs aren’t well-optimized for the job. Even reservoirs that perform adequate deaeration might be secretly weighing down the system and the oil budget.
How can air contamination affect my hydraulic system?
Discussions around contamination usually focus on solid particulates and water. But what happens to a hydraulic system when it becomes contaminated by air?
If not controlled, air contamination targets system components, overall oil condition, and machine efficiency:
Accelerated Oil Aging: Oxygen in the air speeds up the aging of oil.
Varnish / Gel-Like Buildup: Oil aging byproducts like varnish can foul and damage hydraulic system components.
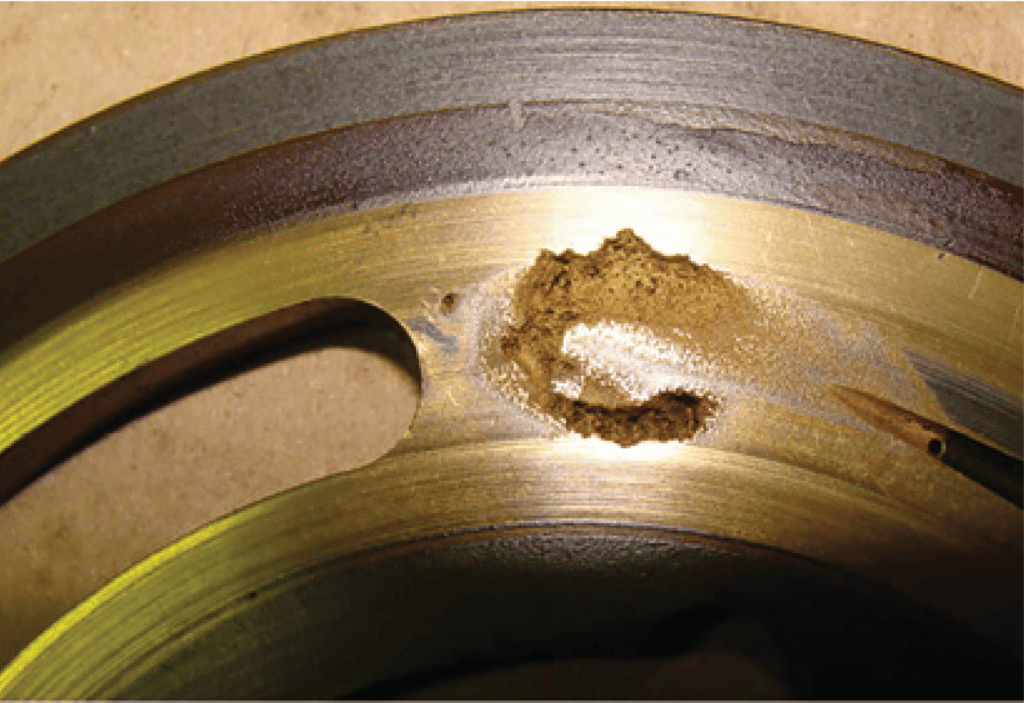
Cavitation: Air bubbles can collapse so violently under high pressure that physical damage occurs.
Microdieseling: Air bubbles may also combust under high pressure, literally burning the surrounding oil & speeding up aging and byproduct formation.
‘Spongy’ Hydraulics: Compressible air can cause delayed responses in the machine’s actions.
Cavitation Damage
How does a hydraulic reservoir influence deaeration?
Unfortunately, it’s impossible to completely eliminate air in a hydraulic system, so best way to handle air in your oil is to influence how the air behaves.
Enabling deaeration involves encouraging any bubbles to coalesce and escape the oil. In a hydraulic system, the hydraulic reservoir is where this deaeration happens.
Ideally, any air bubbles that form in the hydraulic fluid will exit the fluid and disperse into the open headspace of the reservoir.
The key to air removal in the reservoir is reducing fluid turbulence in the reservoir.
Fast, turbulent flow in the reservoir keeps air bubbles circulating and suspended in the fluid for longer. In extreme cases, flow may be high enough that it causes surface disruptions that draw more air into the fluid.
A tank assembly that can reduce the turbulence of flow allows air bubbles to coalesce, rise, and escape from the oil more easily. This can be accomplished with thoughtful tank geometry and carefully selected in-tank filtration.
Eliminating turbulence is also critical for keeping air out of suction lines. The longer air bubbles remain in the reservoir before being drawn into the suction lines, the better their chance of coalescing and escaping the oil. Reducing turbulence is a good way to boost air residence time.
One of the ways that conventional reservoir designs have tried to increase air residence time and combat flow turbulence is by simply making the reservoir bigger.
Increased volume can dampen turbulent flow and increase air residence time…but oversized reservoirs come with some major downsides:
Larger reservoirs require more oil, which drives up oil-related costs.
Bigger, heavier reservoirs increase overall equipment weight and reduce energy efficiency.
With a bigger tank assembly, less space is available for design innovations and other useful features.
How can Tank Optimization and Air Fusion Technology filtration improve my reservoir?
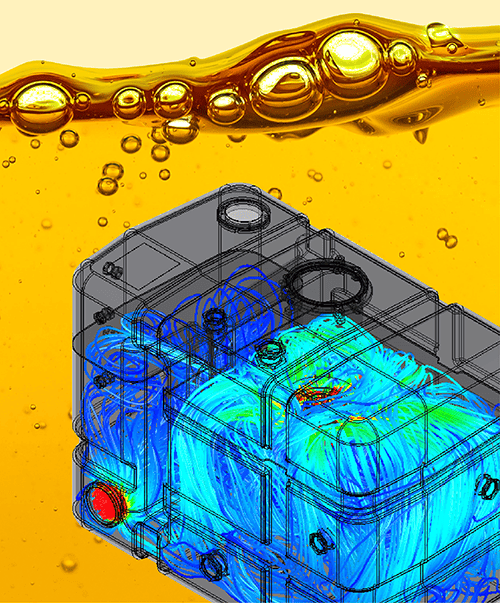
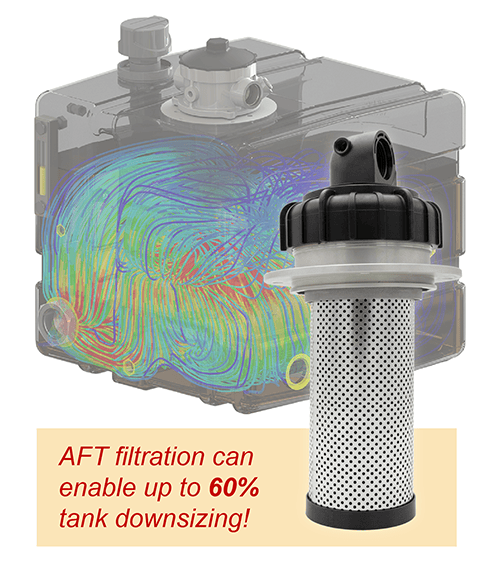
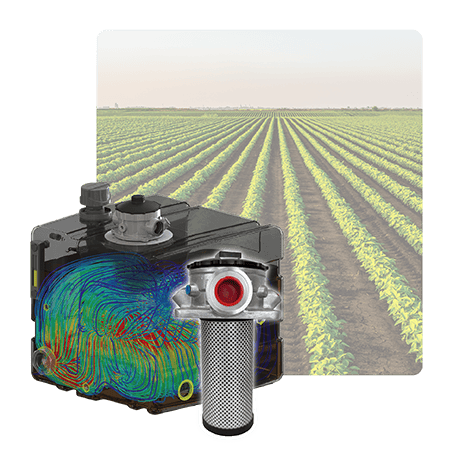
Schroeder Industries’ Tank Optimization uses specialized digital simulations to analyze the existing properties of a tank, identifying inefficiencies in the design. From there, our tank assembly and hydraulic system experts develop a solution that optimizes deaeration and improves overall tank performance.
When paired with purpose-built deaerating filtration, this optimization and redesign process often enables significant reservoir downsizing.
When Tank Optimization meets Air Fusion Technology, reservoir deaeration is maximized.
Tank Optimization analyzes flow, fluid sloshing, structural characteristics, and air residence time—all critical factors in reducing (or potentially worsening) air contamination. Based on the initial analysis, failures of the existing design can be identified and corrected to improve air removal.
See how these real Schroeder Industries clients achieved significant tank assembly downsizing by combining deaerating filters with Tank Optimization:
Tank Optimization + AFT Produces 77.8% Reservoir Reduction
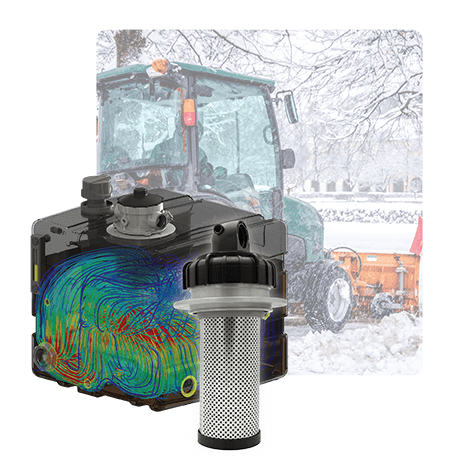
An OEM producing ride-on snow removal equipment, wanting to be more competitive in the market, sought solutions to improve their hydraulic oil cleanliness and optimize their systems.
By combining Tank Optimization with the advanced deaeration of Air Fusion Technology filtration, Schroeder Industries was able to downsize the reservoir from 9 gallons to 2 gallons, allowing the customer to improve their equipment design and become more competitive!
Here’s how Tank Optimization and Air Fusion Technology helped this customer:
Reservoir Downsized by 7 Gallons and 51lbs (77.8%)
Design Improvements: Runs 2x Longer Than Competitor
Tank Optimization + AFT Nearly Halves Reservoir Volume
An OEM manufacturing mobile seed tending equipment sought to assess the performance of their reservoirs and improve their tank design.
This particular customer was producing their own 12-gallon reservoirs in house. Not only could Tank Optimization improve their reservoir design, but any volume reduction would lessen the materials required for manufacturing.
This Tank Optimization, combined with the fixed head Air Fusion Technology configuration (AFTF), was able to downsize the 12 gallon reservoir by almost half.
Here’s how Tank Optimization and Air Fusion Technology helped this customer:
42% Reservoir Downsizing (5 Gallon Reduction)
3,750 Gallons of Oil Saved Across 750 New Units
$40K Reduction in Oil Costs through Tank Optimization
Posted by McKenzie Thorpe on | Comments Off on Compact Diesel Filtration Powerhouse: HDP120
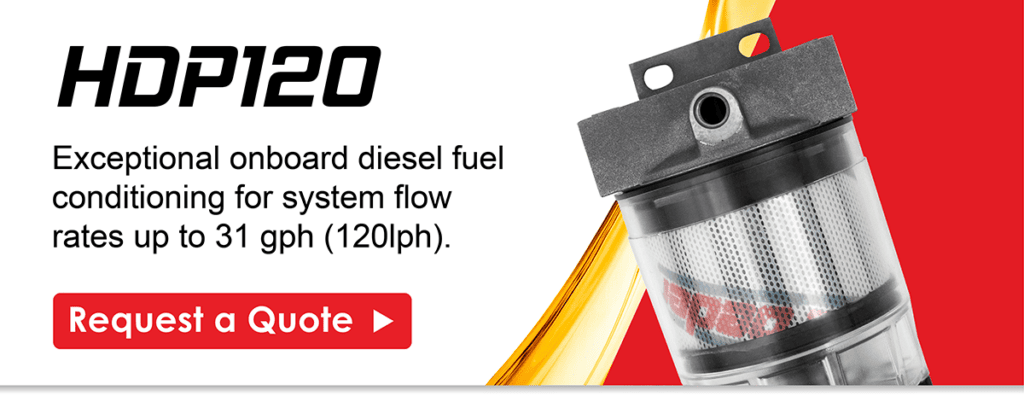
Introducing high-performance diesel filtration for engines up to 31 gph.
Meet the smallest—but certainly not the least—addition to Schroeder’s high-performance onboard diesel fuel filtration lineup.
The HDP120 brings Schroeder’s signature filtration performance to compact, off-highway diesel systems.
Dual Function: Acts as a particulate diesel fuel filter and water separator using the same two-stage element formula found in Schroeder’s larger filters.
High Performance Stability: Provides efficient water separation on the clean side of the filter throughout its entire service life.
Exceptional Filtration: Offers higher diesel filtration efficiency and overall filter life.
Maintenance-Friendly: Simple, fast filter element replacements help your equipment return to duty faster.
Quality Protected: Guaranteed filtration quality; only operable with the use of valid replacement filter elements.
Part of a comprehensive line of onboard diesel fuel filtration solutions.
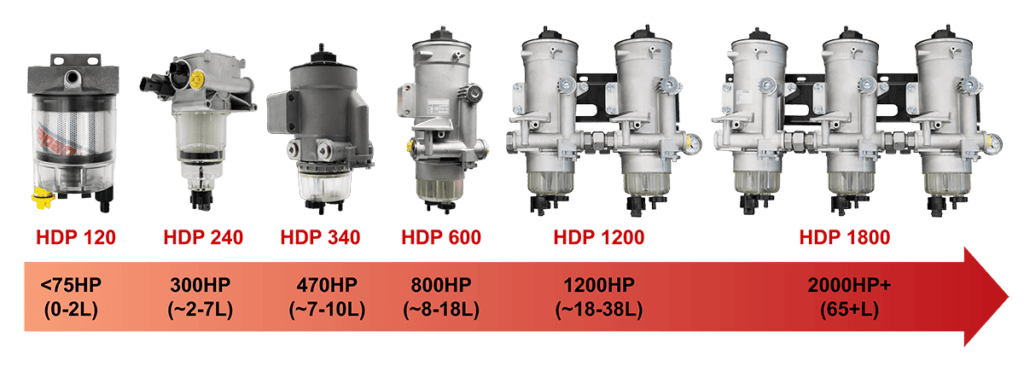
Schroeder Industries has an HDP diesel filter for virtually every engine.
Our exceptional onboard diesel filtration meets stringent modern cleanliness standards and keeps operations moving forward across the globe. Discover solutions serving everything from compact mobile equipment to massive ship engines and power generators:
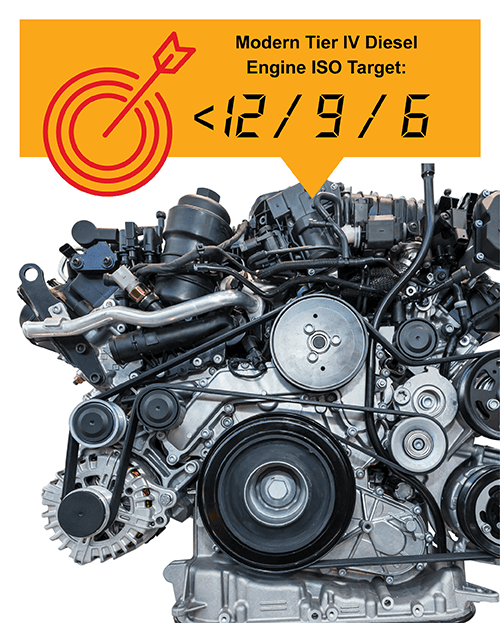
Modern Tier IV diesel engines have exceptionally low tolerance for solid contamination.
The components in a high pressure common rail (HPCR) engines experience incredibly high pressure. Because of this, the cleanliness standard for injected fuel is significantly stricter than hydraulic cleanliness standards.
For injectors and other fuel system components to meet their standard operating lifespan, fuel must meet an ISO Target of <12/9/6 as it enters the injector.
This target represents 16x greater sensitivity than a typical modern hydraulic system!
Replacing a single fuel injector can cost thousands of dollars. Multiply that by a 6 or 8 cylinder engine, and the cost of contamination skyrockets.
Onboard diesel fuel filters are the last line of defense.
Diesel fuel must be filtered at all stages, from the storage and filling phase to final injection. Onboard diesel filtration is the final line of defense for the hyper-sensitive, expensive components that comprise a modern diesel engine.
When selecting a diesel fuel filter, choose wisely!
Talk to the contamination control experts:
Our team of fuel filtration experts can help you determine the right diesel filter for your application.
Posted by McKenzie Thorpe on | Comments Off on The 4 Definitive Qualities of a Good Filter Element
What Makes a Good Filter Element?
Selecting the right hydraulic filter element is one of the most important decisions for maintaining fluid cleanliness, protecting equipment, and maximizing system performance.
Filter elements are at the heart of every hydraulic system. While elements are often treated as a disposable afterthought, their contamination-busting role makes elements absolutely critical for system longevity and performance.
So, if you’re thinking of trying to cut costs with cheap, generic filter elements—think again.
Quality truly matters when it comes to filtration. Whatever you might be saving in element costs, you’ll likely end up losing more in maintenance and repair costs, productivity impacts, and more frequent element replacements.
If using quality filter elements is so important, what should you look for in an element?
There are essentially 4 key metrics by which you can judge the effectiveness of a filter element:
High Beta Efficiency
Minimal Pressure Drop
High Dirt Holding Capacity
Good Beta Stability
Let’s get in to what each of these metrics mean for element performance, and for the integrity of your equipment and fluid assets.
High Beta Efficiency
Filter elements come in a range of different micron ratings—that is, the size of particle the filter is rated to capture.
But, just because a filter has a certain micron rating, that doesn’t necessarily mean that it efficiently captures particles of that size!
Let’s look at an example of two elements tackling solid particles 5 microns and higher:
The percentage of particles of a given size that a filter captures is known as its beta efficiency.
Filter Element A only captures 500/1,000 particles >5µm, which makes its beta efficiency 50% for 5µm. This indicates relatively low efficiency.
Filter Element B, on the other hand, captures 999/1,000 particles >5µm, giving it a beta efficiency of 99% at 5µm. This is considered high efficiency.
Certain elements may be nominally rated for a certain micron rating, but actually have a relatively low beta efficiency. For example, a cellulose media element rated for 5 microns could have a beta efficiency as low as 50%!
When you choose an element, be sure to choose elements with a high beta efficiency to ensure the elements are actually capturing the contamination you are targeting.
Minimal Pressure Drop
In a hydraulic system, maintaining consistency in system pressure is key to efficient system performance.
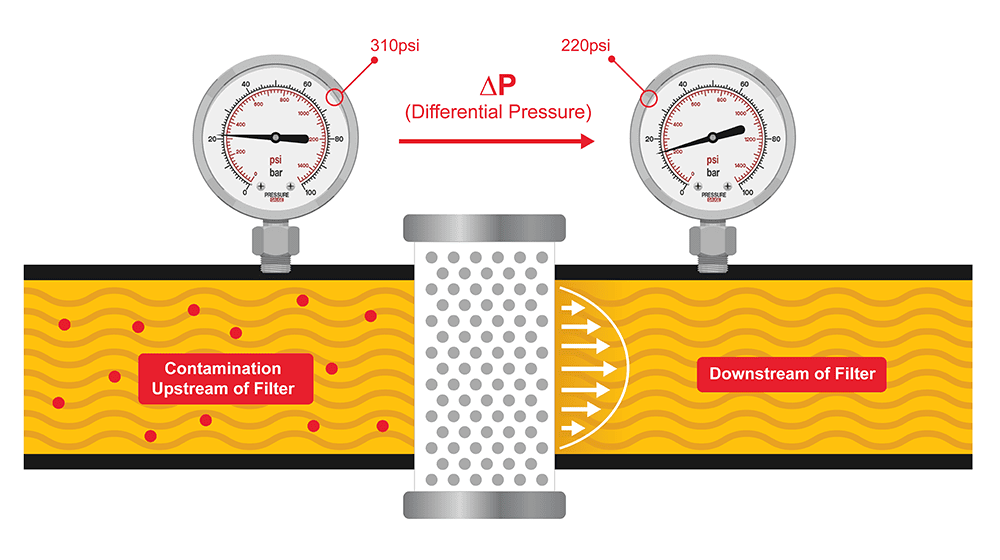
However, filter elements by their nature are somewhat disruptive to pressure in the system. In order to filter out contaminants, elements inherently have to interrupt the flow of fluid to some degree!
Representation of typical system pressure drop downstream of a filter element.
Particle capture/filtration and maintaining system pressure must be carefully balanced.
While removing as much contamination as possible in hydraulic fluid is ideal, the tighter the filtration tolerance of an element (i.e. the smaller its filtration rating), the greater the impact on pressure downstream of the filter.
A high-quality filter element is engineered to balance effective particle capture and system pressure, protecting the machine with minimal impact on its efficiency.
Sometimes, operators may sacrifice filtration performance to ensure that they minimize the pressure drop in their system. In reality, a high-quality element can provide effective filtration without excessively affecting system pressure.
Schroeder Case Study: Minimal Pressure Drop Elements In Action
End users operating frac trailers were deliberately avoiding higher-performance, lower micron-rated elements due to concerns about pressure drop.
But, with the right element, exceptional particle capture with minimal hydraulic system pressure drop is possible!
Schroeder Industries replaced the customer’s existing 40 micron elements with a new 25 micron solution. The 25 micron elements offered similar pressure drop characteristics as the original 40 micron elements, but provided significant improvements in filtration performance.
Here’s how Schroeder’s superior elements helped this customer:
40% Increase in Particulate Removal Efficiency ≥25µm
36% Increase in Element Dirt Holding Capacity
Element Change-Outs & Maintenance Downtime Reduced
Given the role of the filter element in trapping contamination, the amount of solid particulates the element can hold—commonly called ‘dirt holding capacity,’ or ‘DHC’—is another major factor in element quality.
But, the more particles an element captures, the greater the effect on system pressure.
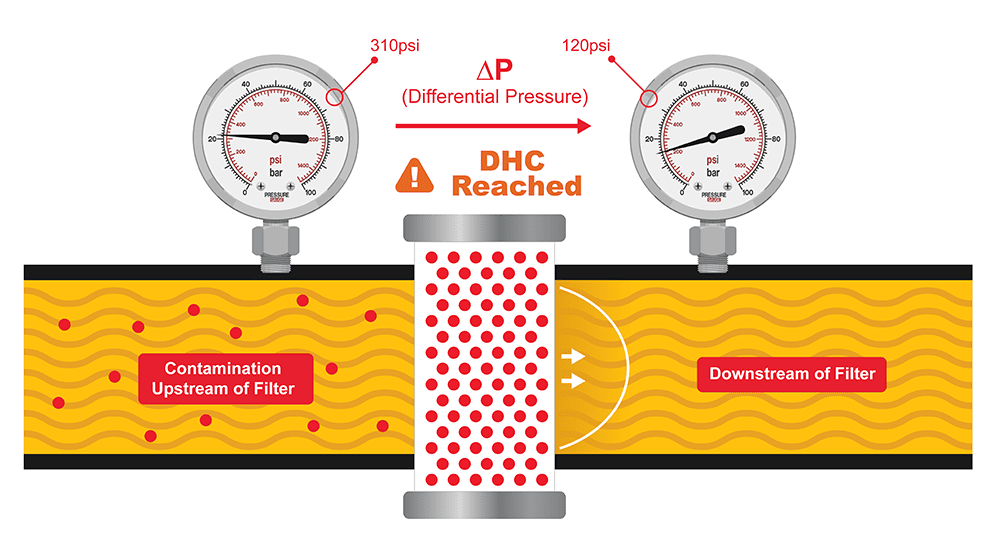
When the element has accumulated enough particles that it causes too much pressure drop downstream of the element, it has reached its DHC and must be changed out for a fresh filter element.
Note how the downstream pressure drop changes from when the element is new to when DHC is reached:
The more contamination a filter element can capture without causing too much pressure drop, the longer the filter can go without maintenance. That’s the key to good DHC!
This not only reduces the costs associated with purchasing new replacement elements, but reduces maintenance-related downtime.
Beta Stability
This aspect of the filter element is closely related to its DHC and efficiency.
Basically, beta stability is the determination of how efficiently the element captures particulates as it approaches its DHC.
For example, if an element rated for 5 microns begins struggling to capture 5 micron particles as it approaches its DHC, that element has poor beta stability.
If an element is rated for 5 microns, it should be capturing 5 micron particles whether the element is at 1% DHC or 99% DHC!
Final Thoughts: Choosing the Best Element
When it comes to selecting the best filter element, the key is a balance between all four of the key traits described above.
An element may have high beta efficiency, meaning it excels at capturing particles of a certain size…but if it loses that ability as it approaches DHC, then it has poor beta stability. If it has a low DHC, then you will need to interrupt operations and purchase replacement elements more often. And so on!
The right filter element finds a balance between all of the above principles, giving you excellent filtration without compromising system efficiency and with minimal maintenance needs.
Want to upgrade your filter elements? Try the BestFit Cross Reference Search Tool!
Premium filter element equivalents for over 42,000 OEM-brand part numbers and counting!
Affordable, high-performance filter elements to fit a wide range of applications
Engineered with Schroeder Industries’ signature quality
Variety of media grades (cellulose, synthetic, water removal, anti-stat, stainless steel, metal mesh)
Posted by McKenzie Thorpe on | Comments Off on What the Worldwide Fuel Charter Means for Your Bulk Fuel
Considering the cost of replacing diesel injectors, it pays to ensure your fuel is clean.
Just one diesel injector can cost hundreds to thousands of dollars to replace. Multiply that by the number of injectors in a 6 or 8-cylinder engine, and the repair costs can take a considerable bite out of a company’s profits!
A well-designed fuel pipeline includes filtration at the transfer, dispensing/filling, and onboard stages. But a successful contamination control plan must begin at the bulk storage stage.
That’s where recommendations from the Worldwide Fuel Charter come into play.
To explain this, we must first review the most critical part of a diesel-driven machine: The injector system.
Diesel injectors are highly sensitive to solid contamination due to their precise engineering and the extreme pressure they experience while operating.
To ensure these expensive, sensitive components are able to reach their standard operating lifespan, they are assigned a very stringent ISO Target of <12/9/6. This target represents 16x greater sensitivity than a typical modern hydraulic system!
While a system of dispensing and onboard filters help diesel fuel reach that stringent target, if the stored fuel is especially contaminated, those filters can become overburdened.
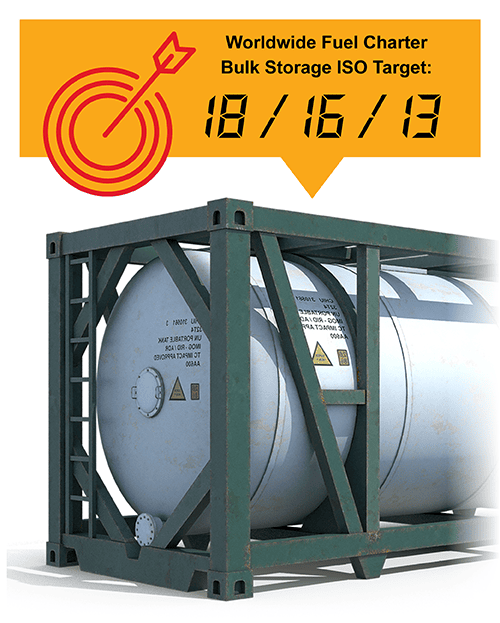
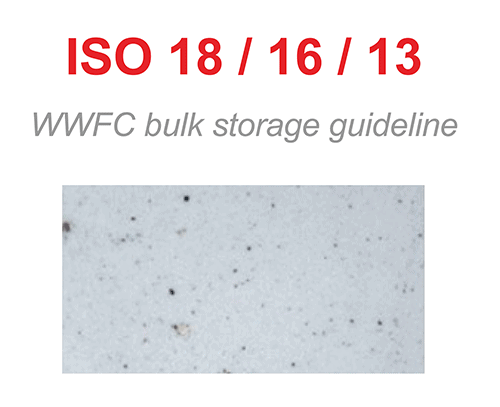
This is why the WWFC suggests a minimum cleanliness target of ISO 18/16/13. By starting with cleaner fuel, the dispensing and onboard filters are not overwhelmed with contamination, allowing them to operate more efficiently and effectively.
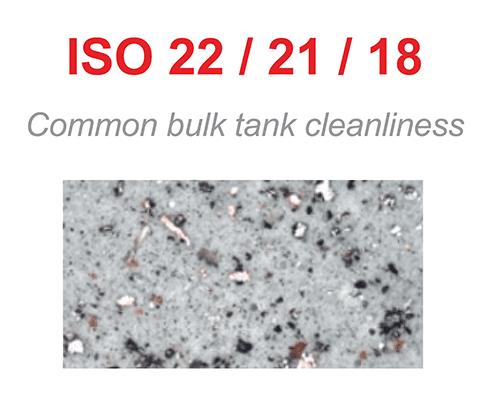
Below are microscopic comparisons of a common condition of bulk diesel tanks versus the WWFC target of ISO 18/16/13.
If you need to reach <12/9/6 to protect your injectors, which bulk fuel condition would you rather start with?
The Costs of Contaminated Fuel
Without taking additional steps to ensure the quality of your bulk diesel, your expenses can skyrocket:
Downtime for increased maintenance and filter replacements/machine repairs will disrupt productivity
Overburdened onboard and dispensing filters will require the purchase of more replacement elements
If the dispensing and onboard filters can’t keep up with the contamination, extremely expensive engine and component damage can occur.
The bottom line: Starting with cleaner bulk fuel can cut costs!
Contamination Vectors to Watch Out For
Understanding how bulk stored fuel becomes contaminated can help you implement the right solutions! Here are some of the primary ways that contamination occurs in storage tanks:
New fuel does not always meet the WWFC standard! There are many opportunities in the supply chain for contamination to occur, so be sure to filter any newly purchased fuel before adding to storage.
Storage tanks may already be contaminated. Ensure that empty storage tanks are properly cleaned before adding new fuel.
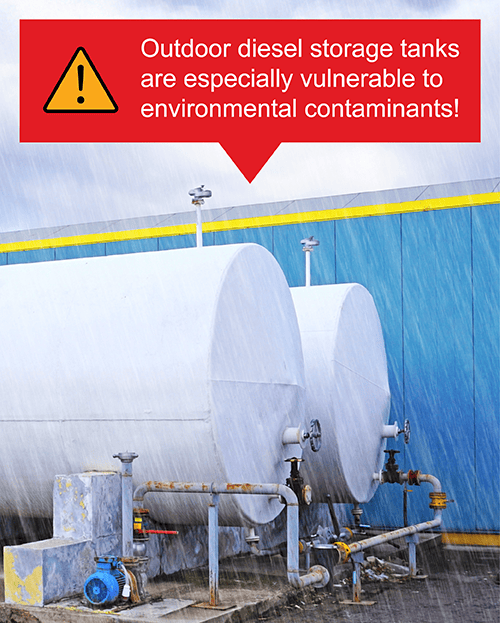
Storage tanks are vulnerable to environmental contaminants. Storage tanks, especially when kept outside, are vulnerable to rain and humidity, pollen and dust, and other environmental factors.
Microbial growth can worsen contamination. ‘Diesel bug’ is a phenomenon where, through a combination of water contamination and bacteria in the tank, thick microbial sludge grows and thrives in the tank.
Bulk Diesel Solutions from Schroeder Industries
Schroeder Industries engineers, manufactures, and delivers a full suite of fuel filtration and polishing solutions!
Here are just two of our favorites:
BDFP – Bulk Diesel Filtration Panel
14 or 25 gpm (53 or 95 L/min)
Combines particulate GHPF filter and coalescing GHCF filter with integrated pump. Powerful performance & straightforward installation in new or existing filtration systems!
Posted by McKenzie Thorpe on | Comments Off on How to Set ISO Cleanliness Targets for Hydraulic Systems
When it comes to contamination, what you don’t know could be costing you.
In hydraulic systems, up to 70%-90% of wear and failure is contamination related!
To keep your equipment functioning properly, slash repair costs, and operate as efficiently as possible, contamination control is essential. The effects of contamination costs tens of thousands, even hundreds of thousands of dollars for industrial operations across the world every day!
Every person dealing with hydraulic equipment, diesel-powered equipment, and even compressed gases should know some contamination basics.
Let’s review solid contamination, ISO Codes, and ISO Targets, some of the most fundamental principles of contamination control.
Recap: Solid Contamination
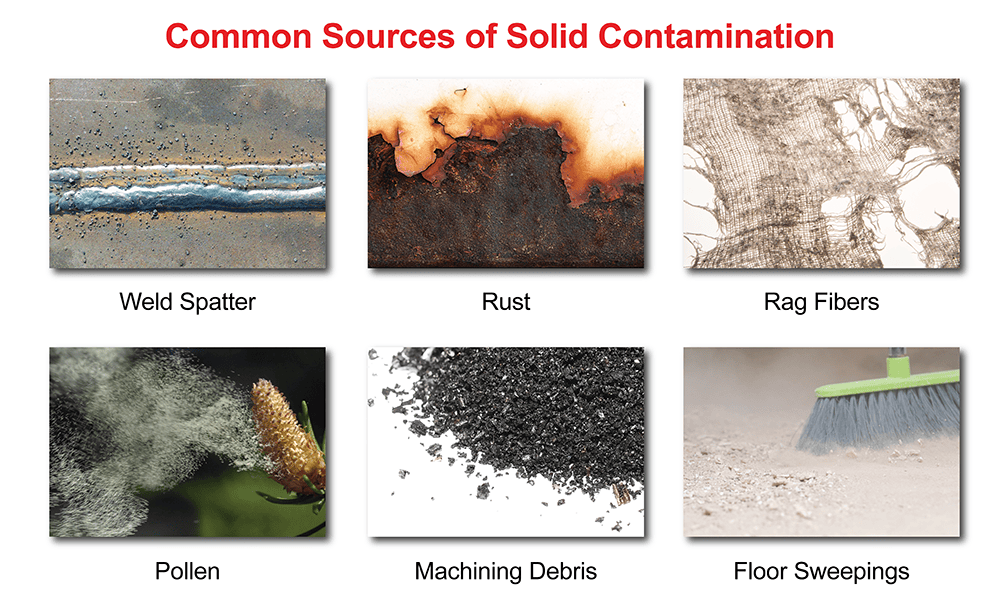
Solid contamination is the most common, and often the most destructive form of contamination in fluid-powered systems. There are countless opportunities for solid contamination to infiltrate hydraulic fluid, diesel fuel, and other operating fluids:
Dust, grit, sand, and other solid particles in the operating environment.
Organic solids such as pollen and debris from trees and other vegetation.
Introduction of ‘new’ fluid that is not adequately filtered. (Never assume that ‘new’ oil or fuel is ‘clean’!)
Machining debris left over from equipment manufacturing and assembly. (This is often called ‘built-in contamination’.)
Solid contaminants are often smaller than the eye can see, but these tiny particles can add up to huge losses in efficiency, productivity, and profit!
In the world of fluid power, solid contaminants are measured in microns, often represented by the symbol ‘µm’. Microns are used to measure particles on the microscopic level.
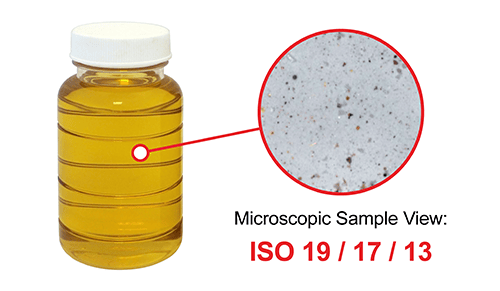
While a sample of hydraulic oil or diesel fuel might look perfectly clean at a glance, under a microscope, the hidden danger becomes obvious. These solid contamination particles may be incredibly small, but their impact on your machines can be massive!
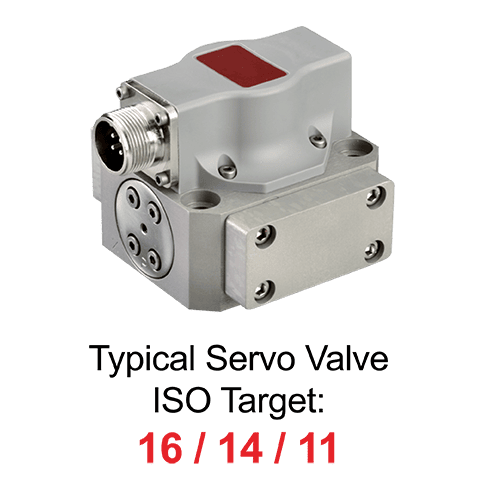
As microscopic particles of solid contamination grind through your system, they gradually wear down critical components like servo valves, pumps, cylinders, injectors, seals, and more.
When these components eventually fail, the repercussions can range from inconvenient, to costly, to catastrophic for productivity and even worker safety!
Knowing how how to measure solid contamination—and how much contamination your system can handle before risking premature failure—is incredibly important.
ISO Codes: Decoding Solid Contamination
The amount of solid contamination in a fluid system or a fluid sample is represented by an ISO Code.
ISO Codes (pronounced ‘eye-so codes’) are numerical codes used to quantify the amount of solid contamination in hydraulic fluid, diesel fuel, process fluid—essentially, any operational fluid!
ISO Codes consist of three numbers, separated by forward slashes. These three numbers represent the amount of solid particles across three different size ranges in the fluid.
Higher numbers in an ISO Code mean more contamination in the fluid!
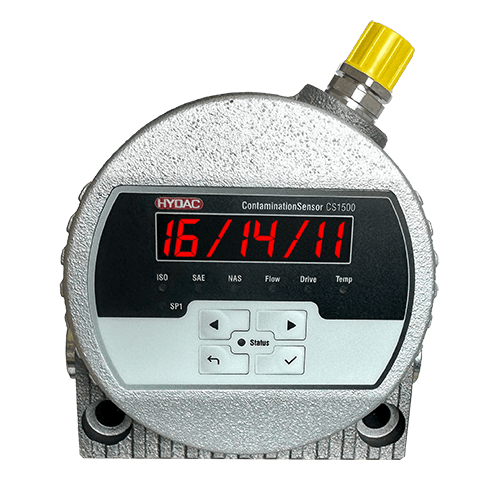
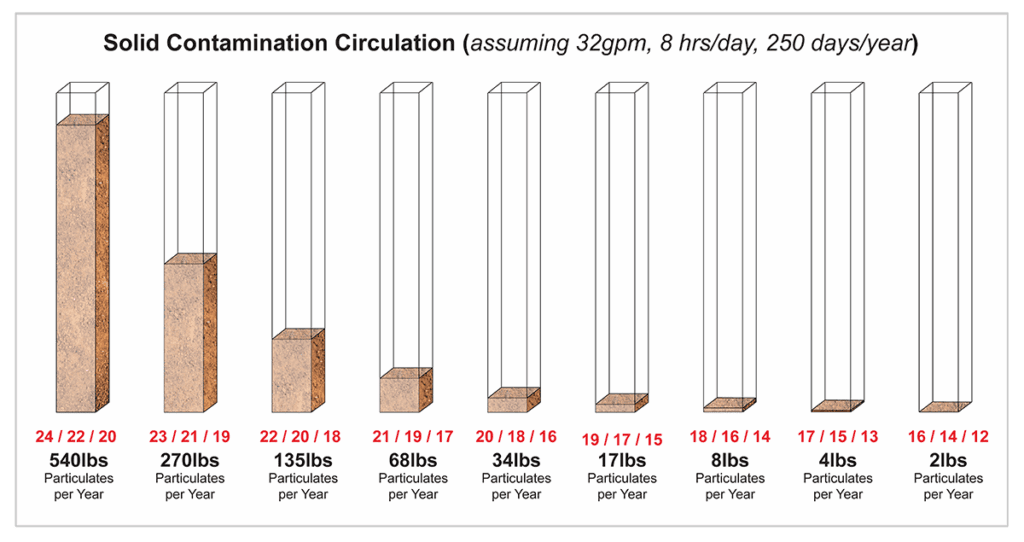
Additionally, with each increase in ISO Class, the amount of contamination is actually doubled. So, if your hydraulic system starts at ISO 16 / 14 / 11, and goes up to ISO 17 / 15 / 12, there istwice as much solid contamination grinding through your system every time you turn it on!
This means that what may seem like a small change in your ISO Code can have huge impacts. Just a few rungs up or down the ISO Class ladder can mean the difference between tens or even hundreds of pounds of solid contamination circulating in your system every year!
If your machine is operating with dirty fluid, this could take years off its life in terms of peak performance. This is why knowing and meeting your machine’s cleanliness targets, also called ISO Targets, is so important!
Tolerances and ISO Targets
ISO Codes are also used to represent part tolerances.
‘Tolerance’ refers to how much contamination a machine component can tolerate and still maintain a ‘normal’ lifespan according to manufacturer guidelines.
Components that are more complex, more sensitive, or located in higher-pressure regions of the fluid circuit, etc. will generally be less tolerant to contamination.
Because tolerance is represented by an ISO Code, an individual component or system’s tolerance is commonly called an ISO Target.
An ISO Target is basically the ISO Code you should aim for in your operating fluid to help your equipment live up to its potential!
Different components within a system may have different tolerances, and thus, different ISO Targets!
The ISO Target for an entire machine or system is based on the component with the lowest tolerance. That way, protection is ensured across the whole system for even the most sensitive component!
How Can I Find My Machine’s ISO Target?
Manufacturer guidelines generally include a minimum ISO Target.
However, a custom assessment could find a target that helps your equipment outlive its expected operational life!
A manufacturer may set a machine’s ISO Target based on a ‘normal’ lifespan for different components.
But, if you can push your fluid cleanliness beyond the manufacturer’s minimum recommendation, it may add years of efficient performance to your machine’s life!
Want to find out if your equipment could go above and beyond its normal operating life?
Talk to the experts at Schroeder Industries! We can provide a comprehensive analysis of your current ISO Targets and contamination control program, and make customized recommendations that help your equipment live up to its full potential.
Tell us about your applications, your equipment, and your operational goals. We’re here to help!
Posted by McKenzie Thorpe on | Comments Off on Top 5 Filtration Innovations of 2025 | Schroeder Industries
Another year of filtration innovation is on the books!
Filtration innovations continue to improve equipment reliability, reduce contamination, and help industries operate more efficiently. At Schroeder Industries, our engineering and product development teams are dedicated to creating advanced filtration solutions that deliver long-term value and keep critical equipment performing at its best.
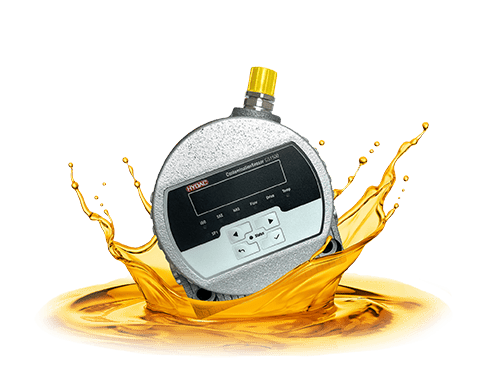
From smarter contamination monitoring to sustainable filtration technologies, 2025 brought several exciting advancements.
If you missed them, here are the Top 5 Filtration Innovations from Schroeder Industries in 2025:
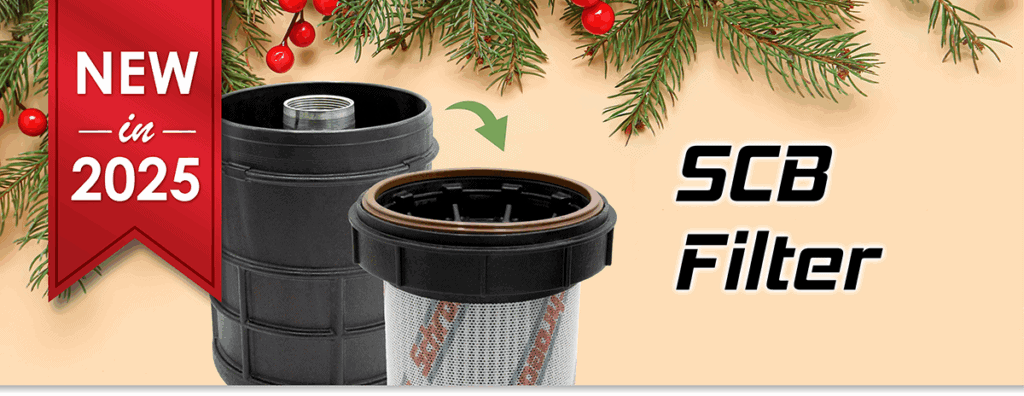
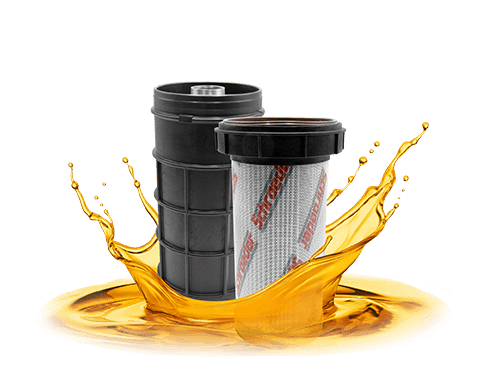
Sustainable Cartridge Bowl (SCB)
A sustainable alternative to conventional spin-on filters, the Sustainable Cartridge Bowl (SCB) helps reduce waste, lower operating costs, and deliver reliable filtration performance without compromising durability.
Waste-Eliminating: Reduces scrap metal waste by more than 90% and oil waste by more than 80% compared to conventional spin-on filters.
Carbon-Cutting: Lowers carbon footprint by more than 80% versus traditional spin-on filters.
Built for Tough Applications: The glass-infused nylon bowl is extensively tested for impact resistance and cyclic pressure performance under extreme temperatures.
Performs Under Pressure: Designed with a burst rating exceeding 600 psi, providing a 4:1 safety factor—twice the safety factor of typical spin-on filters.
Lower Operating Costs: The reusable bowl design reduces replacement costs with every element change-out.
Superior Filtration Performance: High-pleat filter elements deliver lower pressure drop and more effective filtration to help protect critical equipment.
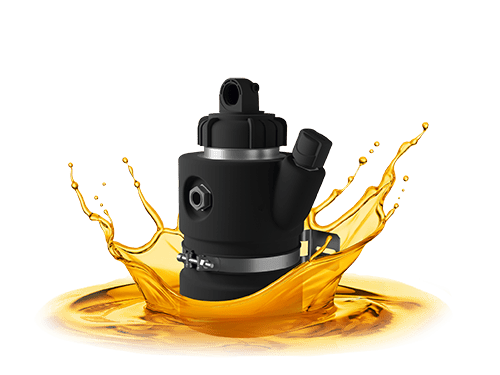
The TNK1C is the most compact reservoir in Schroeder Industries’ TNK Series, delivering durable construction, optimized hydraulic performance, and integrated filtration in a lightweight, all-in-one design.
Durable Construction: The rotomolded reservoir is highly durable, impact-resistant, and designed to maintain its integrity in extreme temperatures.
Optimized Performance: Engineered to improve flow, minimize oil volume, enhance cooling, and support effective hydraulic filtration.
Powered by AFT Technology: Integrated Air Fusion Technology (AFT) provides industry-leading deaeration and effective in-tank filtration for improved fluid cleanliness.
Sustainable Design: The recyclable reservoir requires significantly less energy to manufacture than comparable steel tanks.
Complete Solution: Comes equipped with essential accessories, including gauges, in-tank filters, and air breathers, for simplified installation and operation.
Schroeder Industries’ advanced coalescing fuel filtration system delivers enhanced filtration performance, continuous operation, and durable construction for demanding fuel filtration applications.
Enhanced Filtration Performance: Dual GHCF housings provide up to 2x greater coalescing filtration performance than a single housing configuration.
Versatile Applications: Ideal for both bulk fuel filtration and high-horsepower onboard equipment where reliable fuel cleanliness is critical.
Continuous Operation: Dual filter housings allow one filter to be serviced while the other remains in operation, minimizing downtime during routine maintenance.
Built to Last: Manufactured from high-quality anodized aluminum for long-lasting performance in demanding operating environments.
Compact, Space-Saving Design: Engineered to fit tight installation spaces while supporting applications where reduced weight and space efficiency are important.
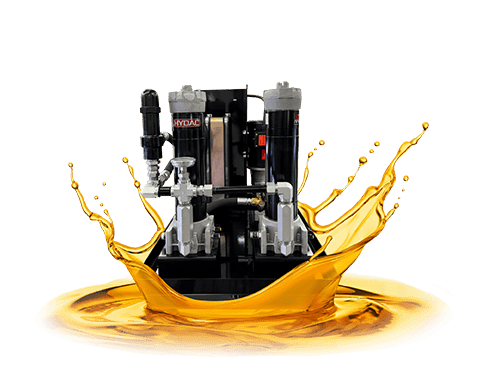
The Gearbox Cooling Skid helps protect gearbox systems by combining effective lubricant filtration with reliable cooling to reduce wear, prevent overheating, and improve equipment reliability.
Comprehensive Protection: Removes solid particulates while cooling lubricating fluid to help protect critical gearbox components.
Prevents Overheating: Cools gearbox lubricants to reduce heat-related component degradation and extend equipment life.
Minimizes Downtime: Designed to address common gearbox vulnerabilities, helping reduce unplanned downtime and costly repairs.
Flexible Cooling Options: Available in both air-cooled and water-cooled configurations to meet a variety of application requirements.
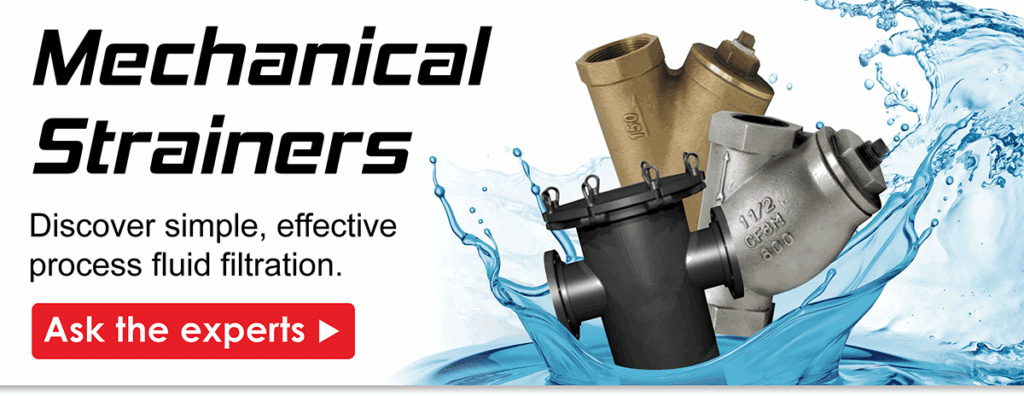
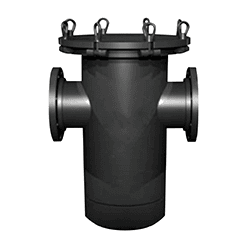
Mechanical strainers play an important role in process filtration by removing larger particles and protecting downstream equipment from contamination and damage. They are commonly used alongside other process filters or as an economical stand-alone solution for applications requiring coarse particle removal.
Mechanical strainers are commonly used in tandem with other process filters, or as an economical stand-alone filtration option for capturing larger particles.
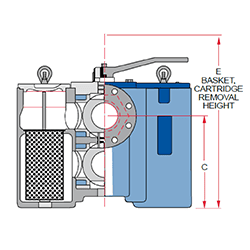
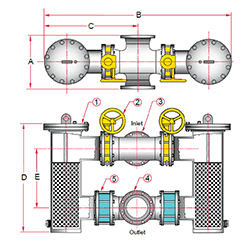
Schroeder Industries recently added a series of mechanical basket strainers and Y-strainers to our process filtration lineup.
With a variety of materials and connection options, there is something for virtually every process application in need of a mechanical strainer!
Which type of mechanical strainer are you looking for?
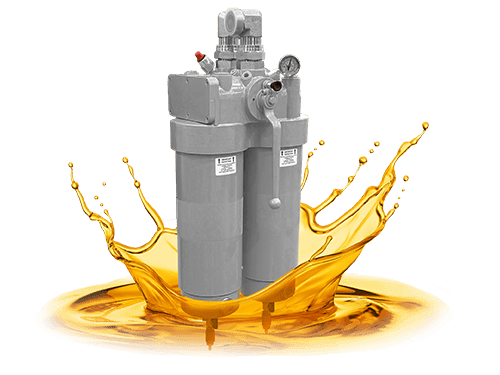
Schroeder Industries first developed the GeoSeal® High-Flow Coalescing Filter (GHCF), a landmark in coalescing filtration. This compact filter is engineered for exceptional particulate and water removal for both onboard applications and in bulk fuel filtration.
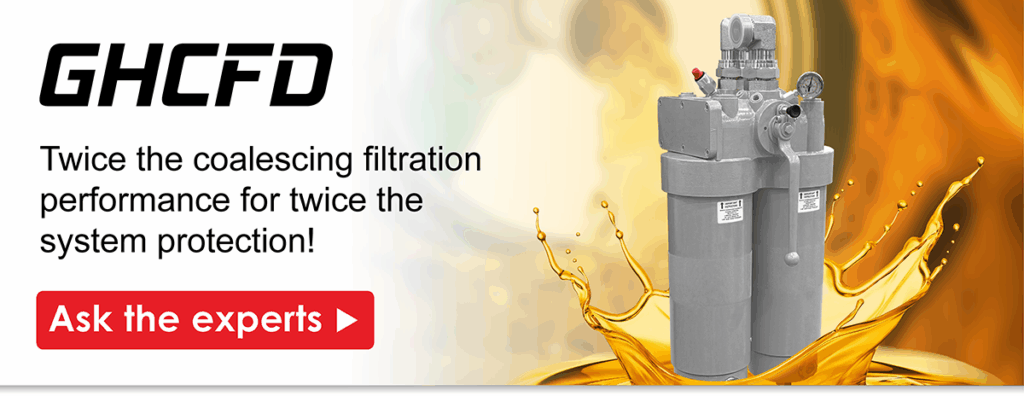
Now, the power of the GHCF is available in a duplex housing option! Introducing: The GHCFD.
Combining two GHCFs in tandem creates a powerful diesel fuel filtration solution that virtually eliminates filter maintenance downtime while providing the same first-rate particulate and water removal.
Exceptional Filtration: Capable of simultaneously filtering out fine particles and water to improve fuel cleanliness.
Versatility: Ideal for large, high-horsepower, onboard applications in industries such as marine, power generation, and oil & gas. Also provides powerful filtration for bulk applications.
Continuous Operation: Dual filter housings allow individual servicing of filters without interrupting operation, eliminating downtime when performing routine filter maintenance.
Durable Construction: Built from high-quality anodized aluminum, ensuring long-lasting performance in the most challenging environments.
Compact and Space-Efficient: Designed to fit within tight spaces, ideal for applications with limited room and in need of weight savings.
Flow Rating (Suction Installations):Up to 1,800 gph (Up to 6,800 L/hr) in center valve position, 900 gph (3,410 L/hr) in the left/right valve position.Flow Rating (Pressure Installations):Up to 50 gpm (189 L/min) in center valve position,Operating Pressure:150 psi (10.3 bar)Min.Yield Pressure:1650 psi (65 bar)Operating Temperature Range:-20° F to 225° F (-29° C to 107° C)Bypass Setting:Blocked for Suction Installations, 40 PSI (2.8 bar) for pressure side installations.Materials of Construction:Filter Assembly: Anodized AluminumSealing Material: FKM & PTFEWeight:54.3 lbs.Element Change Clearance:4.5 inches (114 mm)
Up to 25 gpm (95 L/min) in the left/right valve position.
Max.
Valve: Stainless Steel
(24.6 kg.)
Ask the fuel filtration experts what the GHCFD can do for your application!
Introducing a Waste-Eliminating Spin On Filter Alternative
>90%
reduction in wasted scrap metal
>80%
less hydraulic oil waste
>80%
reduction in CO2 emissions
Spin on hydraulic filters are a popular filtration option. These filters combine the filter housing and element as one complete unit, which can be quickly and easily screwed on and off the hydraulic system.
However, the disposable housing also greatly increases the overall cost per change-out. Additionally, there is massive material waste, as the filter housing is thrown away with the element when a spin on filter is replaced.
Enter the Sustainable Cartridge Bowl filter, or SCB!
This revolutionary filter offers the same spin on convenience, with a reusable housing bowl design. The innovative SCB offers a range of advantages:
More cost-effective element replacement compared to conventional spin-on filters
Cuts down on waste and emissions, including a >90% reduction in scrap metal waste
Discards less oil with each change-out, conserving resources
Powered by filter elements with higher pleat counts and lower pressure drop for superior filtration performance
The SCB’s Signature, Patented Innovation
The material and cost savings of the SCB are made possible through its reusable housing bowl.
The secure sealing and glass-infused, injection-molded nylon bowl provide a durable housing for the high-performance element within.
Robust outer bowl provides re-usability and durability.
The outer portion of the bowl is injection molded plastic, supported by an internal steel tube and flange structure. This results in a lightweight, yet durable housing bowl.
The end-cap of the filter element slides over the bowl, forming a seal along the outer rim and preventing operation without a filter element in place.
Coreless filter element design: higher performance, reduced waste.
The coreless filter element design with plastic caps makes disposal simpler. With support from epoxy-coated wire mesh, pleat stability, efficiency, and dirt holding capacity are increased. These premium filter elements also feature a higher pleat count and lower pressure drop, further improving their performance.
How Does the SCB’s Sustainability Compare to Conventional Spin-Ons
Traditional spin on filters contribute to waste and CO2 emissions in two primary ways: wastedscrap metal, and wasted oil.
This waste takes up landfill space and contributes to emissions released during production.
The SCB filter elements, however, are almost entirely plastic and can be easily crushed for efficient disposal. Between these elements and the reusable housing bowl, scrap metal waste is reduced by ~99%.
Extra oil may become trapped in a typical spin on housing, but the SCB only loses oil which has saturated the filter element.
Waste Reduction Example, per 1,000 spin ons:
M10 (cellulose 10 micron) Spin On
1,966 pounds metal scrap waste
If not properly drained, wastes approximately 450 gallons of oil
CO2 emissions: approximately 10,600lbs of CO2
SCB Coreless Replacement Design
Only 20 pounds of metal scrap waste (epoxy wire)
Total oil volume lost through cartridge change-outs: 57.2 gallons (87% reduction versus conventional spin-on filter)
CO2 emissions: approximately 1,300lbs of CO2 (88% reduction versus conventional spin-on filter)
The signature reusable housing bowl of the SCB isn’t just eco-smart: it’s far more cost effective than typical spin on filters.
With a reusable housing bowl, only the filter element must be replaced, which results in exponential savings after just a few element change-outs. And, with the SCB, the first kit comes with a spare element, meaning the first change-out is already paid for.
Over the lifetime of a given piece of equipment, savings can be substantial!
Contact Schroeder Industries or a verified Schroeder distributor for pricing details.
Increased Revenue in Spare Element ROI Strategy
The average aftermarket filter element retention for OEMs is just ~35%.
However, the Quality Protection built in to every SCB bowl and element prevents the use of subpar third-party elements. Not only does this help the end user protect their vital equipment, it can boost aftermarket retention for OEMs to as high as 100%.
Assuming 1,000 machines are produced per year, with 4 element changes per year, substantial gains in aftermarket revenue are possible through a spare element sales strategy:
For increased aftermarket retention, the SCB also includes private labeling options for the bowl and filter elements. To learn more about Schroeder Industries’ private labeling capabilities, view the Private Labeling Capabilities Form.
Petroleum-Based Fluids:Z-Media® and Anti-Static media (synthetic)High Water Content:All Z-Media® and Anti-Static media (synthetic)Invert Emulsions:10 and 25μ Z-Media® and 10μ Anti-Static media (synthetic)Water Glycols:3, 5, 10 and 25μ Z-Media® and all Anti-Static media (synthetic)
SCB Fluid Compatibility
Flow Rating:50 gpm (190 L/min)Max. Operating Pressure:150 psi (10 bar)Burst Pressure:600+ psi (41.4+ bar)Temperature Range:-20°F to 225°F (-29°C to 107°C)up 250°F (121°C) with VitonReplacement Element Case:6 elements
Posted by McKenzie Thorpe on | Comments Off on Are Spin-On Filters Worth the Cost? The Hidden Trade-Offs
Spin-on filters have become a popular choice for hydraulic filtration because they combine the filter media, housing, base plate, and gasket into one easy-to-replace unit. Their simple, all-in-one design reduces maintenance time and makes filter change-outs quick and convenient.
However, that convenience comes with trade-offs in waste, long-term operating costs, and filtration performance. Before choosing a filtration solution, it’s worth understanding both the advantages and limitations of spin-on filters.
Let’s review the pros and cons of spin-ons!
Spin-On Filters: The Benefits
It’s not for nothing that spin-on filters are popular in hydraulic applications:
User-Friendly Maintenance. Unlike cartridge filters, spin-on filters generally don’t require any special tools during connection or removal from a system. Change-outs and maintenance can be performed more quickly than with a typical cartridge filter due to the all-in-one design.
Lower Up-Front Cost. The price of spin-on filters is lower than the up-front cost of a traditional cartridge-style filter assembly.
Minimal Spillage. The self-contained design of a spin-on filter prevents oil leaks for a more sanitary change-out process.
Spin-On Filters: The Drawbacks
But, while convenience is a helpful quality of spin-ons, their disposable nature has some significant downsides:
Oil & Metal Waste. Due to the all-in-one design of spin-on filters, the entire housing is disposed of along with the element. Not only is any trapped oil discarded, but the metal which forms the spin-on housing, core, and gasket are unrecoverable.
Inefficient Disposal. Spin-on filters cannot be recycled, shredded, or incinerated through normal waste-processing. As a result, spin-on filters eat up landfill space.
Lower Performance. Spin-on filters tend to have lower efficiencies compared to cartridge filter media, which can reduce overall system efficiency.
Counting the Cost of Spin-Ons
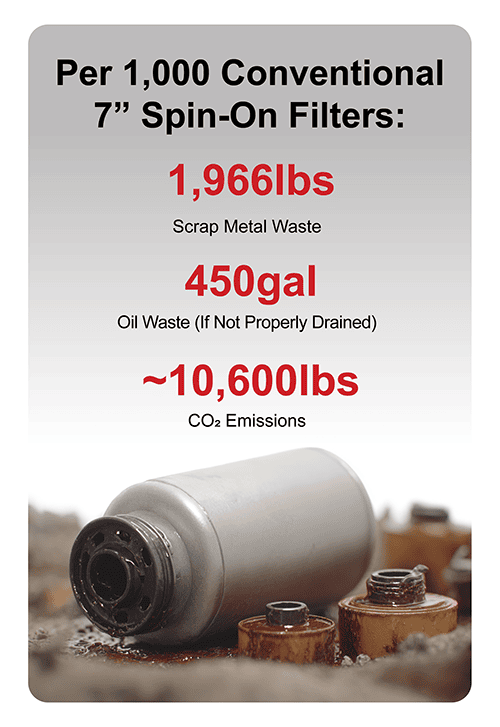
The greatest downside of spin-on filters is the sheer amount of material and oil waste involved. Let’s look at an example of how much waste is produced by a very common spin-on type:
Waste Reduction example, per 1,000 spin ons:
7″M10 (cellulose 10 micron) Spin On
1,966 pounds metal scrap waste
If not properly drained, wastes approximately 450 gallons of oil
CO2 emissions: approximately 10,600lbs of CO2
Millions of spin-on filters are discarded every year, contributing to a staggering amount of unnecessary waste!
Is It Time For A Change?
While spin-on filters are a convenient and effective choice for filtration, the wasteful nature of conventional spin-on technology can’t be ignored.
Between environmental repercussions and potential missed revenue, spin-on filtration technology is long overdue for an upgrade.
Material and oil costs rise with each passing year. With the amount of metal and oil wasted with each spin-on, it’s likely that users could be paying more than they need to for their spin-on filtration.
Could a less wasteful, more cost-effective spin-on alternative not only reduce emissions, but save money for hydraulic-driven operations?
Can the convenience and user-friendliness of spin-ons be combined with the economical, lower-waste benefits of cartridge filters?
Schroeder Industries thinks so.
A More Sustainable Alternative to Spin-On Filters
A low-waste, cost-effective, high-performance spin-on alternative is coming soon. Stay tuned for Schroeder Industries’ most game-changing innovation yet!
Get Notified of the Launch!
Register for our mailing list to receive an email notification when this revolutionary spin-on filter alternative formally launches: