Comments Off on Compact Diesel Filtration Powerhouse: HDP120
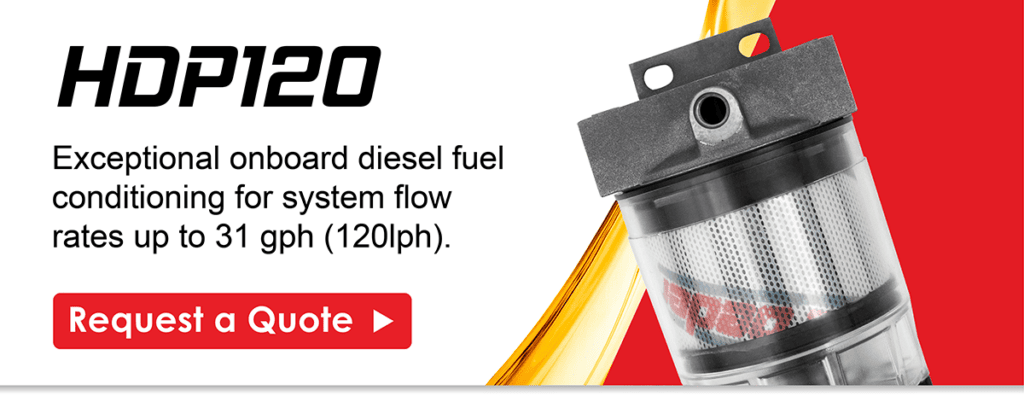
Introducing high-performance diesel filtration for engines up to 31 gph.
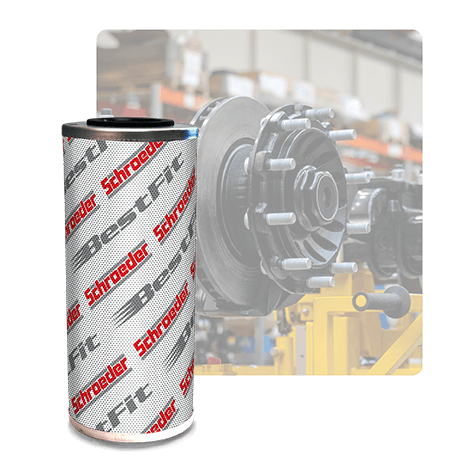
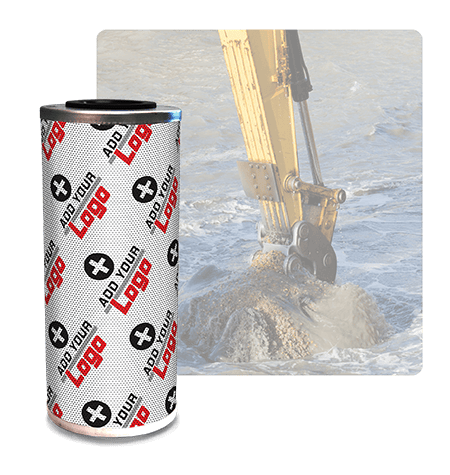
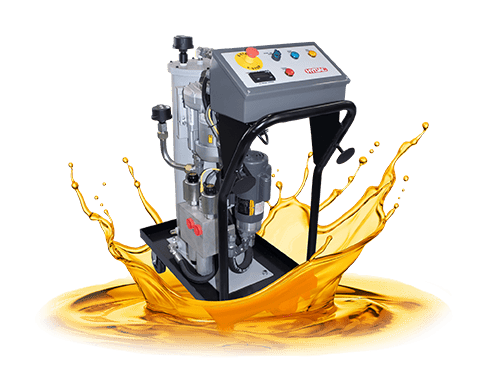
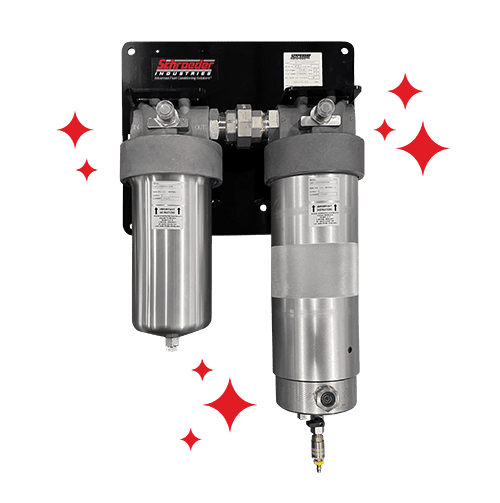
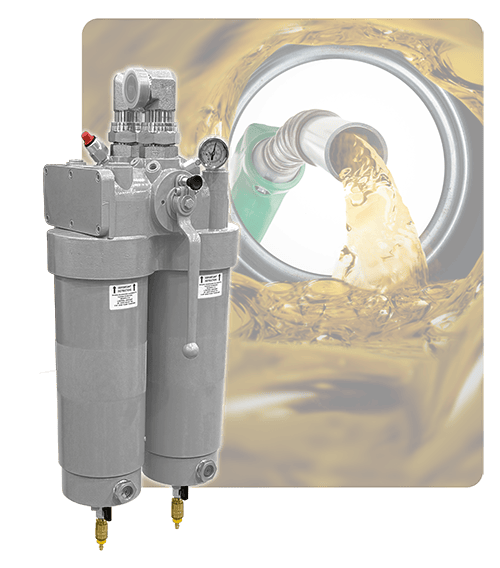
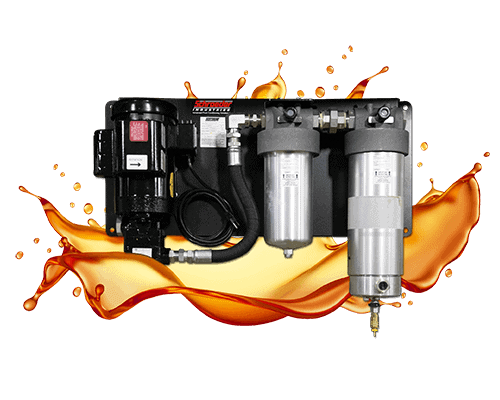
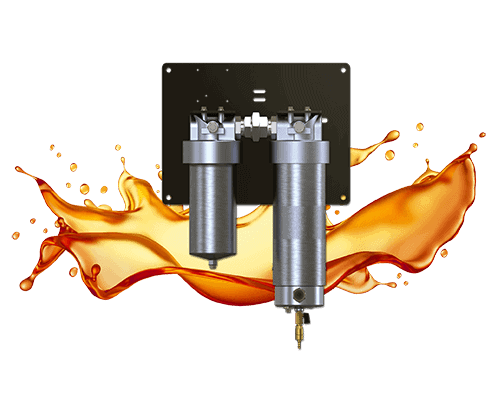
Meet the smallest—but certainly not the least—addition to Schroeder’s high-performance onboard diesel fuel filtration lineup.
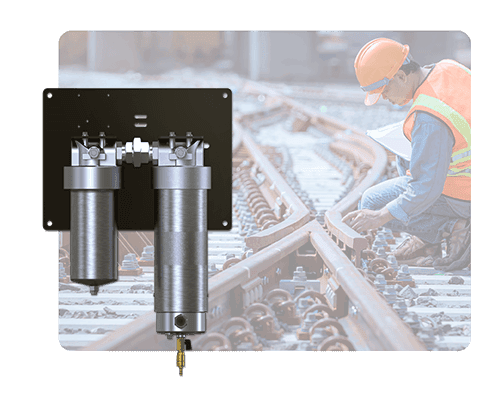
The HDP120 brings Schroeder’s signature filtration performance to compact, off-highway diesel systems.
Dual Function: Acts as a particulate diesel fuel filter and water separator using the same two-stage element formula found in Schroeder’s larger filters.
High Performance Stability: Provides efficient water separation on the clean side of the filter throughout its entire service life.
Exceptional Filtration: Offers higher diesel filtration efficiency and overall filter life.
Maintenance-Friendly: Simple, fast filter element replacements help your equipment return to duty faster.
Quality Protected: Guaranteed filtration quality; only operable with the use of valid replacement filter elements.
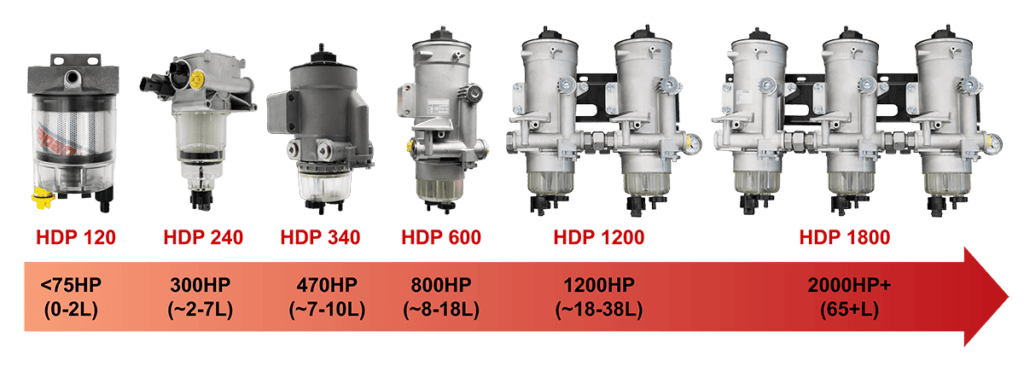
Part of a comprehensive line of onboard diesel fuel filtration solutions.
Schroeder Industries has an HDP diesel filter for virtually every engine.
Our exceptional onboard diesel filtration meets stringent modern cleanliness standards and keeps operations moving forward across the globe. Discover solutions serving everything from compact mobile equipment to massive ship engines and power generators:
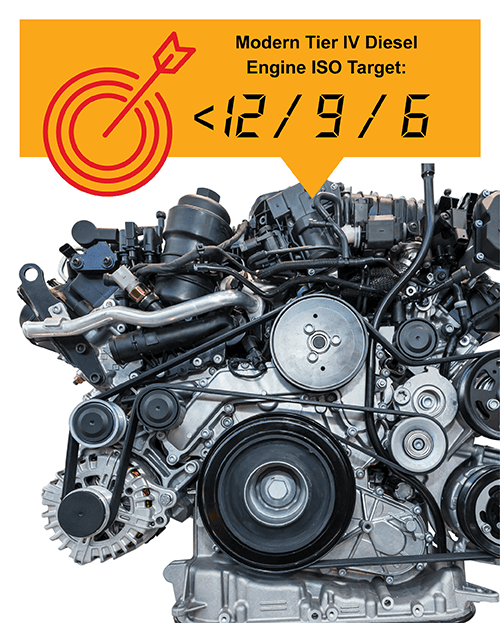
Modern Tier IV diesel engines have exceptionally low tolerance for solid contamination.
The components in a high pressure common rail (HPCR) engines experience incredibly high pressure. Because of this, the cleanliness standard for injected fuel is significantly stricter than hydraulic cleanliness standards.
For injectors and other fuel system components to meet their standard operating lifespan, fuel must meet an ISO Target of <12/9/6 as it enters the injector.
This target represents 16x greater sensitivity than a typical modern hydraulic system!
Replacing a single fuel injector can cost thousands of dollars. Multiply that by a 6 or 8 cylinder engine, and the cost of contamination skyrockets.
Onboard diesel fuel filters are the last line of defense.
Diesel fuel must be filtered at all stages, from the storage and filling phase to final injection. Onboard diesel filtration is the final line of defense for the hyper-sensitive, expensive components that comprise a modern diesel engine.
When selecting a diesel fuel filter, choose wisely!
Talk to the contamination control experts:
Our team of fuel filtration experts can help you determine the right diesel filter for your application.
When a buyer is looking for a replacement filter element, the first thing they usually look for is the micron rating of an element. A selection of elements for a given micron rating don’t look obviously different from each other.
So, to cut expenses, buyers may lean towards the lowest cost option.
Here’s why that’s a mistake.
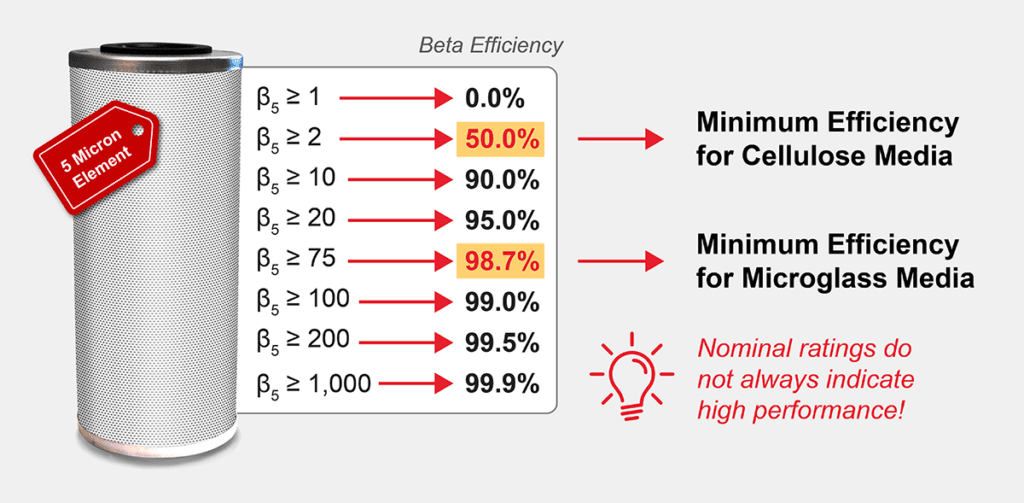
When an element is classified as a 5 micron element, etc, this is known as a nominal rating. To earn a nominal rating, a filter element needs to meet a minimum filtration efficiency requirement for particles of that size.
However, the minimum efficiency can vary greatly depending on the materials used in the filter element! For elements constructed with cellulose media, the minimum efficiency requirement is only 50%.
Microglass media elements need to meet a much higher threshold. An efficiency of 98.7% is required to meet the nominal rating for a given particle size.
Would you trust an element whose efficiency might be as low as 50% to protect your equipment?
Probably not!
But if the nominal rating is not a reliable indicator of performance, what should a buyer look for?
A filter element’s beta efficiency is determined through laboratory testing in a controlled filtration environment.
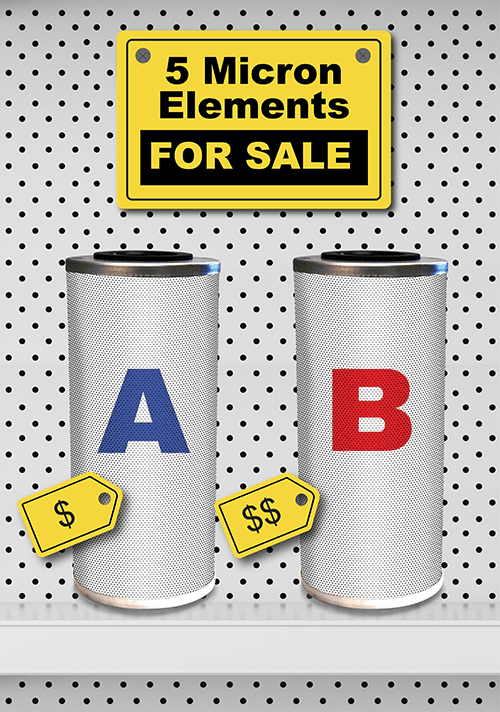
Let’s compare two elements in an example filtration scenario:
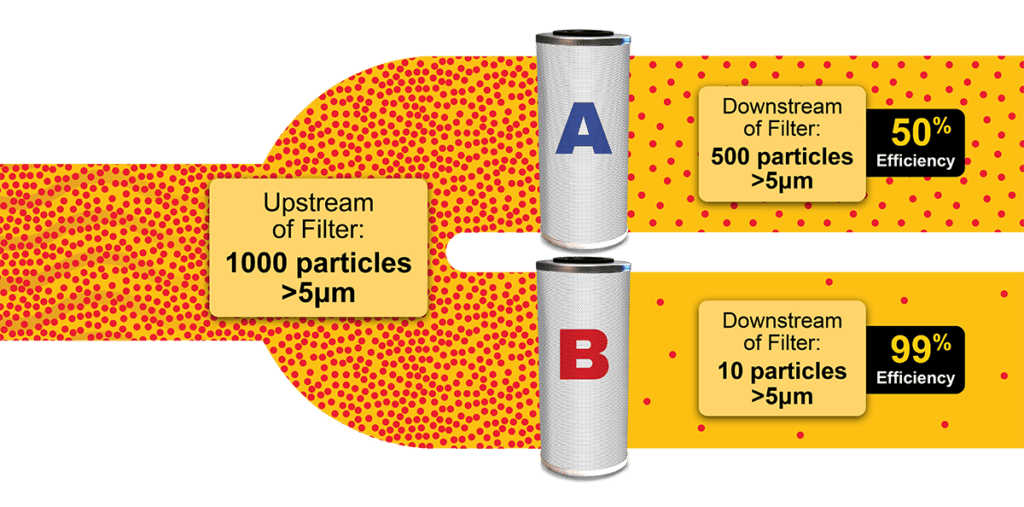
With 1,000 particles 5 microns or larger upstream of the element, we can see how efficiently our two elements capture particulates.
Filter Element A only captures 500/1,000 particles >5µm, which makes its beta efficiency 50% for 5µm. This indicates relatively low efficiency.
Filter Element B, on the other hand, captures 990/1,000 particles >5µm, giving it a beta efficiency of 99% at 5µm. This is considered high efficiency.
In Summary:
Nominal Rating:
Indicates that a filter element meets minimum filtration performance requirements. Should not be treated as a definitive measure of element performance.
Absolute Rating:
A precise measurement of filter element performance, based on beta efficiency. More accurately describes element performance versus a nominal rating.
How do I find the absolute rating of a filter element?
For more information about absolute rating and other performance metrics, try searching for more information on the manufacturer’s website.
Absolute ratings are often expressed in manufacturing literature as beta ratios, which are a kind of shorthand for beta efficiency. Check out the video below to learn how to convert a beta ratio into a percentage!
The filtration experts at Schroeder Industries have delivered filtration success for customers across a wide spectrum of industries. Whatever the scope or focus of your application, our qualified filtration specialists can work with your team to help determine the most effective replacement filter element solution for your application.
Through private labeling and Quality Protection, we also help OEM’s deliver on their brand’s performance promises for end users.
Due to pressure drop and cost-related concerns, end users operating frac trailers were reluctant to adopt higher-performance, smaller micron-rated elements despite their existing 40 micron elements inadequate performance.
To satisfy customer concerns and increase their system protection, Schroeder Industries engineered a new element specifically designed for the types of filter commonly seen in these frac trailer applications.
Head to head testing proved that the new 25 micron Schroeder BestFit element option greatly outshines the customer’s current elements while remaining cost-competitive!
Here’s how Schroeder Industries’ Element Technology helped this customer:
An OEM producing marine dredging equipment was being blamed for premature field failures, and grappling with increased warranty claims.
The culprit behind the failures was actually the substitution of low-quality filter elements by the end users. These elements failed to effectively control contamination, resulting in rapid component degradation and unexpected failures.
To reinforce the OEM’s warranty protection and encourage appropriate element usage, Schroeder Industries partnered with the OEM to establish a private labeled element program.
Here’s how Schroeder Industries’ Element Technology helped this customer:
Comments Off on Can Better Water Control Protect Your Hydraulic Oil?
Water contamination can sink your productivity and drown your budget.
Solid contamination is the most common type of contaminant, but water contamination can be just as damaging.
Water contamination in hydraulic oil occurs when dissolved, emulsified, or free water enters the fluid and reduces lubrication, promotes corrosion, and accelerates component wear.
The risk is constant in applications that utilize large quantities of water or are exposed to weather and ambient humidity.
Uncontrolled water contamination damages equipment and productivity for any hydraulic system operating in such environments:
Water contamination lowers oil lubricity, which accelerates component wear.
Rusting, corrosion, and oxidation can occur as water interacts with internal system components.
Physical damage such as macro-pitting (spalling) and micro-pitting can occur in cylinders, gears, and other parts.
Ultimately, total machine failures may occur, forcing operations to halt.
Paying to replace oil or hiring a third party oil reclamation service can seriously undermine your profits—not to mention the cost of equipment repairs and lost productivity
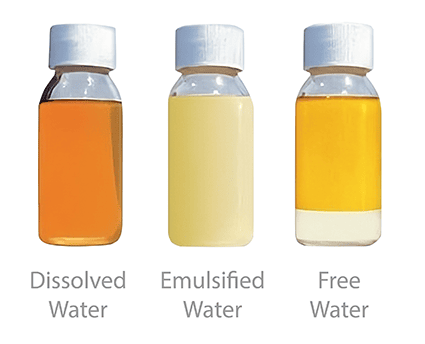
Water contamination comes in three forms, with different levels of severity for your equipment:
Free Water: The worst kind of water contamination. Free water is a separate, visible layer of water that forms when hydraulic oil exceeds 100% saturation.
Emulsified Water: As saturation approaches 100%, small water droplets are visibly suspended in the fluid, giving it a cloudy appearance. While not as inherently damaging as free water, emulsified water is a clear warning sign of contamination approaching a critical level.
Dissolved Water: Considered the least harmful state of water contamination. However, extreme temperature changes can cause dissolved water to separate and become free water.
Changes in temperature can cause water to change form in your system, moving between these three states.
Regardless of how the water in your oil is behaving at one moment, it can go from relatively harmless to increasingly damaging when temperatures start to shift! This means that controlling all water contamination at all times is vital.
Is my operation vulnerable to water contamination?
Virtually any industry can experience some level of water contamination. However, some industries stand out as particularly vulnerable:
Marine: The risk of water contamination when operating on rivers, lakes, and oceans goes without saying! Additionally, swings in temperature in these outdoor environments can cause free water to form, flooding the system with the most damaging state of water.
Pulp & Paper: High volumes of water are required in pulp processing and paper production. In these applications, water contamination is a common pain point.
Steel: High heat applications mixed with high-pressure cleaning spray-downs creates intense humidity. Temperature changes in steel plants can easily trigger condensation of water into the hydraulic reservoirs.
Water contamination can infiltrate reservoirs and equipment in multiple ways.
Damaged seals, a rainy and humid climate, high-pressure water streams used in the cleaning process, and poor bulk oil storage are some common vectors for water contamination. Because water contamination can come from so many places, creating a plan to combat it can be challenging.
How can I prevent water contamination in my hydraulic oil?
Step 1: Test your oil to determine saturation levels.
If you suspect water contamination, it’s important to test your oil. When you know the saturation levels you’re dealing with, it’s easier to develop a strategy for water removal.
Saturation sensors are a great way to detect water contamination in real time. Lab testing is even better, since more sophisticated testing methods can expose other contamination-related problems in your fluid.
Step 2: Examine your equipment and operating environment for vulnerabilities.
Knowledge is power! Finding out where the water contamination is originating from can help prevent it.
Water may be entering via worn seals, loose reservoir caps, poor bulk storage practices, and other variables you can control.
However, many operations may face ambient humidity, big temperature swings, and the unavoidable need for water in their manufacturing process. When a potential source of water contamination can’t be controlled, the best defense is to continuously extract the contamination from your hydraulic oil.
Step 3: Implement water removal filtration tools.
Once you’ve determined how much water you’re dealing with, and where it might be coming from, the next step is filtration. Depending on the amount and frequency of water contamination, there are various tools at your disposal.
Specialized water-removal filter media can absorb smaller quantities of water. Multi-stage filtration housings can allow you to implement different media types to target both water and solid particulate contamination at once.
Large reservoirs and high contamination levels require more specialized equipment. Dehydrating filtration systems are designed to extract free water, as well as a large portion of dissolved water from the fluid.
Step 4: Continuously monitor your fluid condition.
Even with filtration in place, it’s important to implement a strategy for monitoring saturation levels in your oil at all times. Saturation sensors are useful for determining if your dehydrating filtration solution is performing adequately. These sensors can also warn of sudden influxes of water contamination, allowing remedial measures before contamination-driven damage can run rampant.
Many modern saturation sensors include digital connectivity for remote monitoring and reporting, which keeps you informed of your fluid condition in real time, wherever you are.
Schroeder Industries offers a variety of tools and solutions for water removal.
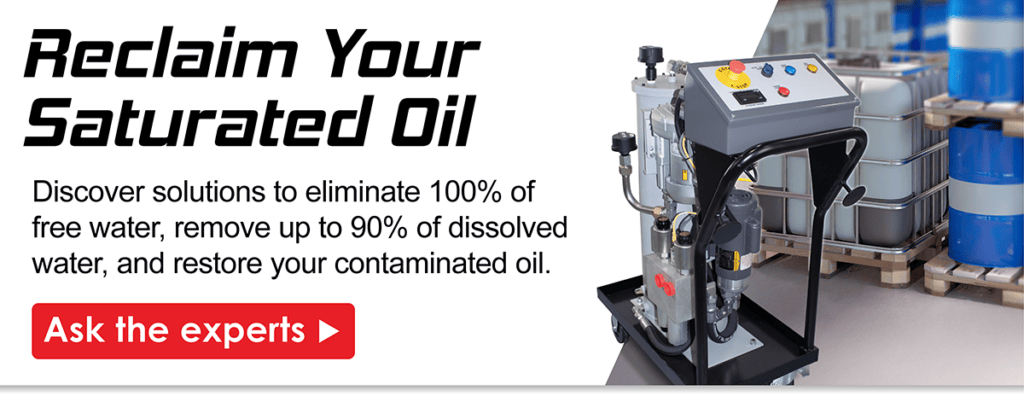
Our Triton Dehydration Stations offer proven performance for oil reclamation in larger reservoirs and high contamination scenarios.
These units are engineered to eliminate 100% of free water and up to 90% of dissolved water by leveraging a patented mass-transfer dehydration technology.
Here’s how Triton Dehydration Stations helped these customers save substantial quantities of oil:
TDS-A Saves Tens of Thousands in Oil-Related Expenses for Injection Molding Equipment
A plastic packaging operations was experiencing high levels of water contamination in their injection molding equipment’s hydraulic reservoir.
The customer was spending tens of thousands of dollars per month on oil recycling costs and new oil purchases.
Schroeder Industries deployed a TDS-A unit to dehydrate their oil, as well as extract any particulate contamination, to ensure operational reliability slash the customer’s oil-related expenses.
Here’s how the TDS-A helped:
16/14/12 ISO Code Reached; Cleaner Than Customer’s ‘New’ Oil
$25-30k USD Saved Per Month on Oil-Related Expenses
220gal of Hydraulic Oil Reclaimed in Just Two Days
TDS-E Saves Pulp & Paper Manufacturer $10K Per Month in Oil-Related Expenses
A manufacturer in the pulp & paper market required additional water removal capacity in their power generation turbine reservoir.
While the operator tried to implement a non-Schroeder dehydration unit, it was unable to keep up with the high volume of water infiltrating the reservoir.
To allow the customer to test the performance of the TDS-E, Schroeder Industries enrolled them in the rental equipment program to prove the unit’s effectiveness.
Here’s how the TDS-E helped:
Rental Program Provides Affordable Access
TDS-E Provides Exceptional Oil Reclamation with Minimal Maintenance
Comments Off on Roll-Off Cleanliness: The Proven Way to Prevent Equipment Failure
When equipment fails prematurely, contamination is often to blame.
For OEMs, premature failures may mean paying out for a costly warranty claim—and, in some cases, exposure to legal liability. Not only do these failures cost the OEM, but they massively inconvenience the end user, and can undermine the manufacturer’s brand reputation.
To reduce the chances of premature failures, every OEM should uphold a high standard of roll-off cleanliness. Fluid filtration is a key aspect of roll-off cleanliness.
How Fluid Contamination Becomes Built-In Contamination
‘Built-in’ contamination refers to contamination that infiltrates a new machine during the assembly and testing process, prior to final delivery to the end user.
Built-in contamination is commonly caused by contaminated components. Metallic fragments lingering after the machining process, or even ambient dust from poor storage and handling practices, can prematurely sideline a machine.
Dirty hydraulic fluid and diesel fuel used to test and fill a new machine can also deliver damaging contamination into the system!
Modern hydraulic and diesel fuel systems have increasingly stringent cleanliness requirements for fluid.
For a modern hydraulic system, the typical standard of cleanliness is an ISO reading of 16/14/11.
Modern Tier IV diesel systems experience higher pressure and contain components with greater sensitivity, so fuel entering the injectors should be less than ISO 12/9/6. That’s 16x more restrictive than the modern hydraulic standard!
You should never assume that your stored fuel or hydraulic fluid is clean, even if it is ‘new!’
‘New’ hydraulic fluid has been found to contain contamination levels as high as 32 times the recommended ISO cleanliness levels for modern systems.
Diesel fuel that has been ‘safely’ stored could be accumulating high levels of water contamination in the background, triggering microbial growth and generating solid contamination within the tank.
If a manufacturer fills the hydraulic and fuel tanks of a machine with contaminated fluid, they are setting the equipment, the end user, and themselves up for failure.
The moment the machine leaves the assembly line with dirty fluid, contaminants begin dealing damage throughout the system.
End users may experience:
Premature Equipment Failure
Impacts to Productivity
Worker Safety Hazards
OEM consequences may include:
Costly Warranty Claims
Legal Liability
Damaged Brand Reputation
To prevent this fluid-borne contamination, any and all operating fluids should be examined and filtered prior to ever touching a machine. As an extra precaution, the equipment’s systems should be flushed and filtered before final delivery as well.
Filtration Solutions for Roll-Off Cleanliness
Schroeder Industries understands the importance of setting end users up for success through roll-off cleanliness. We offer a variety of filtration solutions and diagnostic tools that ensure your equipment is putting its best foot forward from a cleanliness standpoint when it leaves the assembly line.
Diagnostic tools like the TFC are used for establishing ISO counts for fluids in real-time. With particulate shape and size recognition software, the TFC can even provide clues as to where contaminants may be originating from.
Lightweight, hand-held units like the HFS-15 provide the same powerful filtration as a filter cart system with unprecedented mobility. Units with onboard particle counters are available.
Offline filtrations systems such as Schroeder’s array of filter carts (including the MFS, FS, and AMFS) allow for flexibility and mobility. They can act as kidney loop systems for flushing systems, or provide filtration as fluid is transfered into the system.
Ranging from streamlined-but-reliable basic cart systems to advanced systems with onboard particle counting and recording capabilities, these filter carts ensure the cleanliness of fluid within the equipment and can be customized for your specific needs.
Schroeder’s Fuel Filtration division specializes in coalescing and particulate filtration for diesel fuel.
Products like the BDF, GHCF, and more provide superior filtration at every stage of the fuel supply chain, including during transfer, point of fueling, and kidney loop circulating filtration for bulk storage tanks.
Fuel filtration carts like the BDFC combine our world-class fuel filters with integrated pumps, hoses, and a mobile cart chassis.
These turn-key, complete systems offer increased flexibility and enable easy transitions from application to application around a manufacturing plant or storage facility.
Comments Off on The 4 Definitive Qualities of a Good Filter Element
What Makes a Good Filter Element?
Selecting the right hydraulic filter element is one of the most important decisions for maintaining fluid cleanliness, protecting equipment, and maximizing system performance.
Filter elements are at the heart of every hydraulic system. While elements are often treated as a disposable afterthought, their contamination-busting role makes elements absolutely critical for system longevity and performance.
So, if you’re thinking of trying to cut costs with cheap, generic filter elements—think again.
Quality truly matters when it comes to filtration. Whatever you might be saving in element costs, you’ll likely end up losing more in maintenance and repair costs, productivity impacts, and more frequent element replacements.
If using quality filter elements is so important, what should you look for in an element?
There are essentially 4 key metrics by which you can judge the effectiveness of a filter element:
High Beta Efficiency
Minimal Pressure Drop
High Dirt Holding Capacity
Good Beta Stability
Let’s get in to what each of these metrics mean for element performance, and for the integrity of your equipment and fluid assets.
High Beta Efficiency
Filter elements come in a range of different micron ratings—that is, the size of particle the filter is rated to capture.
But, just because a filter has a certain micron rating, that doesn’t necessarily mean that it efficiently captures particles of that size!
Let’s look at an example of two elements tackling solid particles 5 microns and higher:
The percentage of particles of a given size that a filter captures is known as its beta efficiency.
Filter Element A only captures 500/1,000 particles >5µm, which makes its beta efficiency 50% for 5µm. This indicates relatively low efficiency.
Filter Element B, on the other hand, captures 999/1,000 particles >5µm, giving it a beta efficiency of 99% at 5µm. This is considered high efficiency.
Certain elements may be nominally rated for a certain micron rating, but actually have a relatively low beta efficiency. For example, a cellulose media element rated for 5 microns could have a beta efficiency as low as 50%!
When you choose an element, be sure to choose elements with a high beta efficiency to ensure the elements are actually capturing the contamination you are targeting.
Minimal Pressure Drop
In a hydraulic system, maintaining consistency in system pressure is key to efficient system performance.
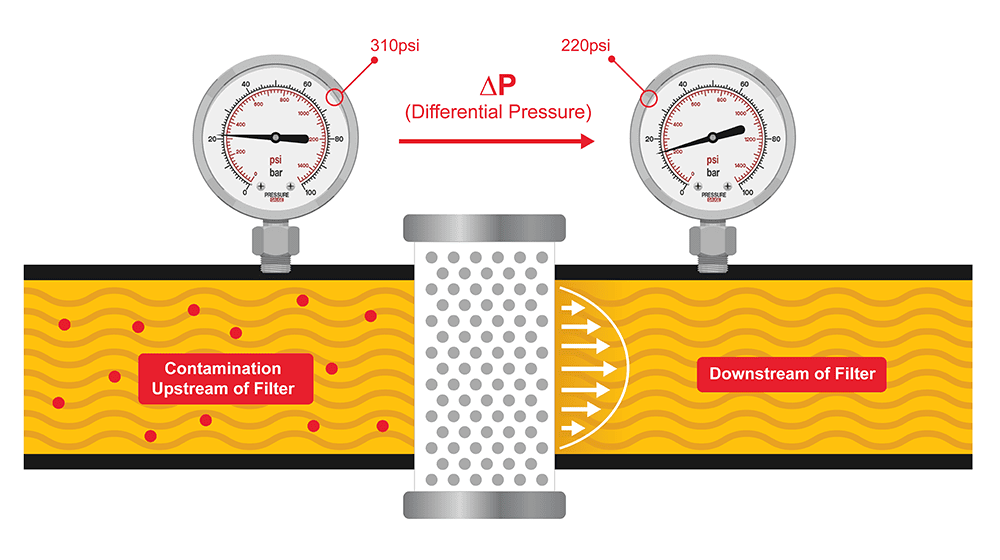
However, filter elements by their nature are somewhat disruptive to pressure in the system. In order to filter out contaminants, elements inherently have to interrupt the flow of fluid to some degree!
Representation of typical system pressure drop downstream of a filter element.
Particle capture/filtration and maintaining system pressure must be carefully balanced.
While removing as much contamination as possible in hydraulic fluid is ideal, the tighter the filtration tolerance of an element (i.e. the smaller its filtration rating), the greater the impact on pressure downstream of the filter.
A high-quality filter element is engineered to balance effective particle capture and system pressure, protecting the machine with minimal impact on its efficiency.
Sometimes, operators may sacrifice filtration performance to ensure that they minimize the pressure drop in their system. In reality, a high-quality element can provide effective filtration without excessively affecting system pressure.
Schroeder Case Study: Minimal Pressure Drop Elements In Action
End users operating frac trailers were deliberately avoiding higher-performance, lower micron-rated elements due to concerns about pressure drop.
But, with the right element, exceptional particle capture with minimal hydraulic system pressure drop is possible!
Schroeder Industries replaced the customer’s existing 40 micron elements with a new 25 micron solution. The 25 micron elements offered similar pressure drop characteristics as the original 40 micron elements, but provided significant improvements in filtration performance.
Here’s how Schroeder’s superior elements helped this customer:
40% Increase in Particulate Removal Efficiency ≥25µm
36% Increase in Element Dirt Holding Capacity
Element Change-Outs & Maintenance Downtime Reduced
Given the role of the filter element in trapping contamination, the amount of solid particulates the element can hold—commonly called ‘dirt holding capacity,’ or ‘DHC’—is another major factor in element quality.
But, the more particles an element captures, the greater the effect on system pressure.
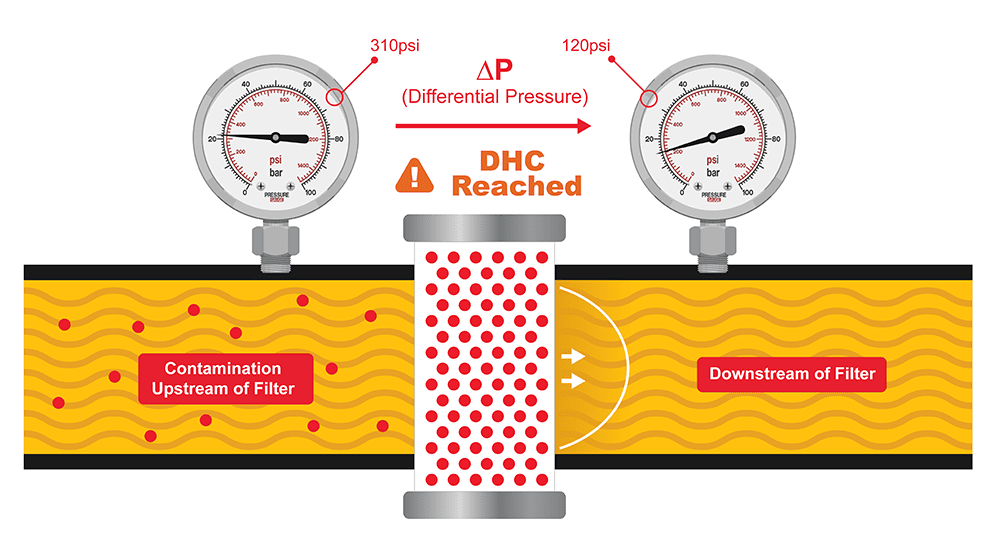
When the element has accumulated enough particles that it causes too much pressure drop downstream of the element, it has reached its DHC and must be changed out for a fresh filter element.
Note how the downstream pressure drop changes from when the element is new to when DHC is reached:
The more contamination a filter element can capture without causing too much pressure drop, the longer the filter can go without maintenance. That’s the key to good DHC!
This not only reduces the costs associated with purchasing new replacement elements, but reduces maintenance-related downtime.
Beta Stability
This aspect of the filter element is closely related to its DHC and efficiency.
Basically, beta stability is the determination of how efficiently the element captures particulates as it approaches its DHC.
For example, if an element rated for 5 microns begins struggling to capture 5 micron particles as it approaches its DHC, that element has poor beta stability.
If an element is rated for 5 microns, it should be capturing 5 micron particles whether the element is at 1% DHC or 99% DHC!
Final Thoughts: Choosing the Best Element
When it comes to selecting the best filter element, the key is a balance between all four of the key traits described above.
An element may have high beta efficiency, meaning it excels at capturing particles of a certain size…but if it loses that ability as it approaches DHC, then it has poor beta stability. If it has a low DHC, then you will need to interrupt operations and purchase replacement elements more often. And so on!
The right filter element finds a balance between all of the above principles, giving you excellent filtration without compromising system efficiency and with minimal maintenance needs.
Want to upgrade your filter elements? Try the BestFit Cross Reference Search Tool!
Premium filter element equivalents for over 42,000 OEM-brand part numbers and counting!
Affordable, high-performance filter elements to fit a wide range of applications
Engineered with Schroeder Industries’ signature quality
Variety of media grades (cellulose, synthetic, water removal, anti-stat, stainless steel, metal mesh)
Comments Off on What the Worldwide Fuel Charter Means for Your Bulk Fuel
Considering the cost of replacing diesel injectors, it pays to ensure your fuel is clean.
Just one diesel injector can cost hundreds to thousands of dollars to replace. Multiply that by the number of injectors in a 6 or 8-cylinder engine, and the repair costs can take a considerable bite out of a company’s profits!
A well-designed fuel pipeline includes filtration at the transfer, dispensing/filling, and onboard stages. But a successful contamination control plan must begin at the bulk storage stage.
That’s where recommendations from the Worldwide Fuel Charter come into play.
To explain this, we must first review the most critical part of a diesel-driven machine: The injector system.
Diesel injectors are highly sensitive to solid contamination due to their precise engineering and the extreme pressure they experience while operating.
To ensure these expensive, sensitive components are able to reach their standard operating lifespan, they are assigned a very stringent ISO Target of <12/9/6. This target represents 16x greater sensitivity than a typical modern hydraulic system!
While a system of dispensing and onboard filters help diesel fuel reach that stringent target, if the stored fuel is especially contaminated, those filters can become overburdened.
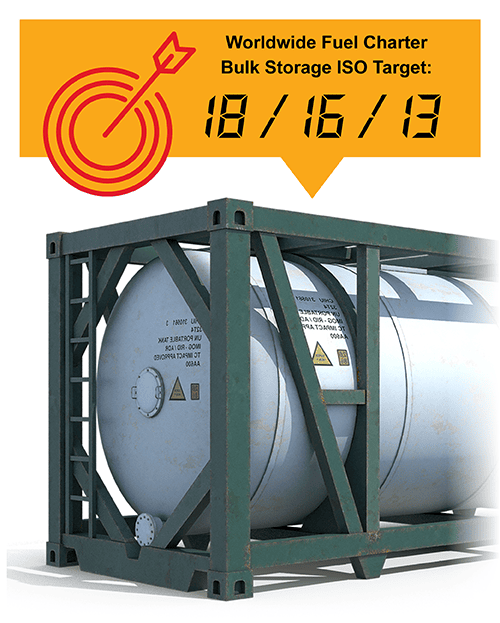
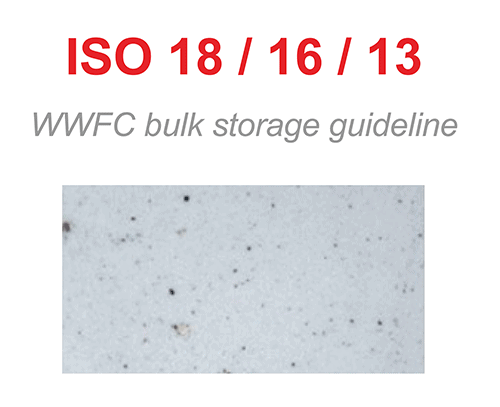
This is why the WWFC suggests a minimum cleanliness target of ISO 18/16/13. By starting with cleaner fuel, the dispensing and onboard filters are not overwhelmed with contamination, allowing them to operate more efficiently and effectively.
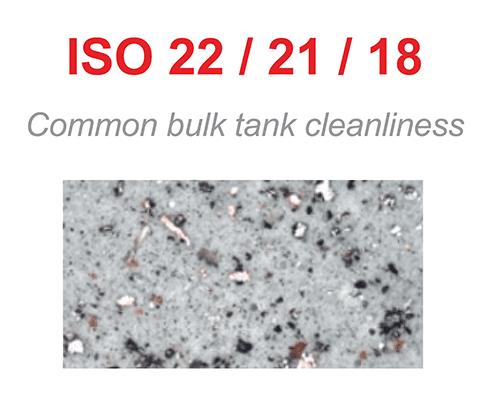
Below are microscopic comparisons of a common condition of bulk diesel tanks versus the WWFC target of ISO 18/16/13.
If you need to reach <12/9/6 to protect your injectors, which bulk fuel condition would you rather start with?
The Costs of Contaminated Fuel
Without taking additional steps to ensure the quality of your bulk diesel, your expenses can skyrocket:
Downtime for increased maintenance and filter replacements/machine repairs will disrupt productivity
Overburdened onboard and dispensing filters will require the purchase of more replacement elements
If the dispensing and onboard filters can’t keep up with the contamination, extremely expensive engine and component damage can occur.
The bottom line: Starting with cleaner bulk fuel can cut costs!
Contamination Vectors to Watch Out For
Understanding how bulk stored fuel becomes contaminated can help you implement the right solutions! Here are some of the primary ways that contamination occurs in storage tanks:
New fuel does not always meet the WWFC standard! There are many opportunities in the supply chain for contamination to occur, so be sure to filter any newly purchased fuel before adding to storage.
Storage tanks may already be contaminated. Ensure that empty storage tanks are properly cleaned before adding new fuel.
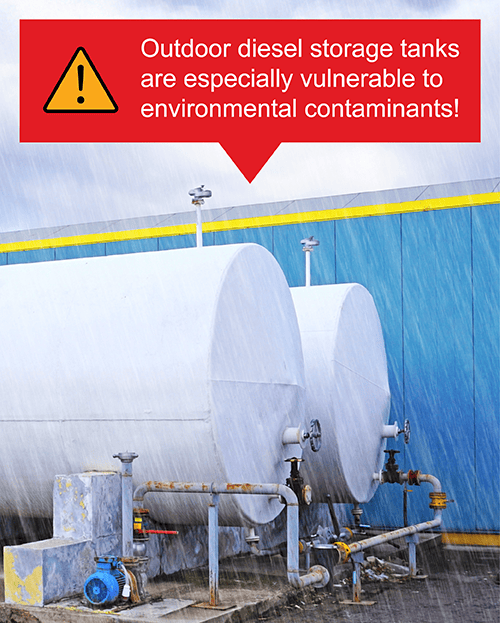
Storage tanks are vulnerable to environmental contaminants. Storage tanks, especially when kept outside, are vulnerable to rain and humidity, pollen and dust, and other environmental factors.
Microbial growth can worsen contamination. ‘Diesel bug’ is a phenomenon where, through a combination of water contamination and bacteria in the tank, thick microbial sludge grows and thrives in the tank.
Bulk Diesel Solutions from Schroeder Industries
Schroeder Industries engineers, manufactures, and delivers a full suite of fuel filtration and polishing solutions!
Here are just two of our favorites:
BDFP – Bulk Diesel Filtration Panel
14 or 25 gpm (53 or 95 L/min)
Combines particulate GHPF filter and coalescing GHCF filter with integrated pump. Powerful performance & straightforward installation in new or existing filtration systems!
Schroeder Industries first developed the GeoSeal® High-Flow Coalescing Filter (GHCF), a landmark in coalescing filtration. This compact filter is engineered for exceptional particulate and water removal for both onboard applications and in bulk fuel filtration.
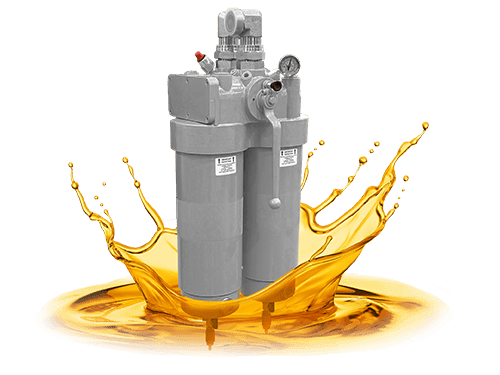
Now, the power of the GHCF is available in a duplex housing option! Introducing: The GHCFD.
Combining two GHCFs in tandem creates a powerful diesel fuel filtration solution that virtually eliminates filter maintenance downtime while providing the same first-rate particulate and water removal.
Exceptional Filtration: Capable of simultaneously filtering out fine particles and water to improve fuel cleanliness.
Versatility: Ideal for large, high-horsepower, onboard applications in industries such as marine, power generation, and oil & gas. Also provides powerful filtration for bulk applications.
Continuous Operation: Dual filter housings allow individual servicing of filters without interrupting operation, eliminating downtime when performing routine filter maintenance.
Durable Construction: Built from high-quality anodized aluminum, ensuring long-lasting performance in the most challenging environments.
Compact and Space-Efficient: Designed to fit within tight spaces, ideal for applications with limited room and in need of weight savings.
Comments Off on Oil Analysis: Protect Equipment & Prevent Downtime
When you think about it, a hydraulic machine is a bit like a human body.
Oil analysis provides insight into the health of hydraulic equipment much like a blood test helps assess the health of the human body.
A hydraulic machine is surprisingly similar to the human body. The motor and pump act as the equipment’s heart, circulating oil throughout the hydraulic system much like blood flowing through a person’s veins. When someone is feeling unwell or monitoring an ongoing medical condition, blood testing provides critical insight into what is happening inside the body and helps guide the appropriate care.
In the same way, oil analysis begins with a fluid sample to evaluate equipment health and identify potential problems related to contamination, fluid condition, and wear.
Contaminants and varnish circulating through the oil can contribute to equipment inefficiency, component wear, failure, and reduced service life. In fact, it is estimated that more than 70% of hydraulic system failures are related to fluid contamination. Fuel and process fluids can also be susceptible to damaging contamination.
Schroeder’s Oil Analysis Program offers a simple way to stay on top of the health of your equipment!
Whether your operation has only a handful of machines, or you manage a massive fleet, Schroeder Industries offers an array of accurate lab testing services and easy digital tracking that keep you informed of your machine’s health.
Advanced laboratory testing provides accurate insights. Our expert testing encompasses a variety of critical fluid health factors.
Multiple test kit options. Schroeder Industries offers three standard testing options, ranging from just the essential fluid values to more in-depth insights.
Receive early warnings on fluid condition. Our testing services will advise you when your fluid parameters fall outside industry standards or customized targets/baselines, allowing you to enact preventative maintenance before downtime or failure occurs.
Receive personalized support from the experts in fluid health. Our fluid condition experts can help you interpret your results and recommend corrective and preventative measures, improving your equipment’s performance and longevity.
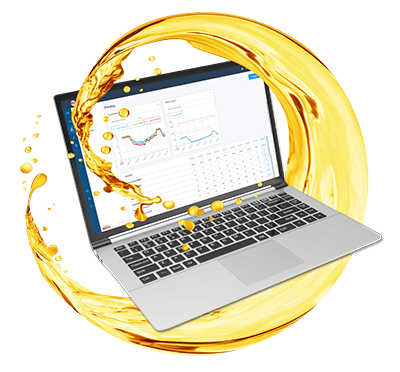
Easy fluid test report management through the Fluid Care Portal. Grappling with paper reports and spreadsheets can make tracking fluid condition trends challenging. This user-friendly web application makes monitoring your fluid health simple, no matter the number of machines you operate.
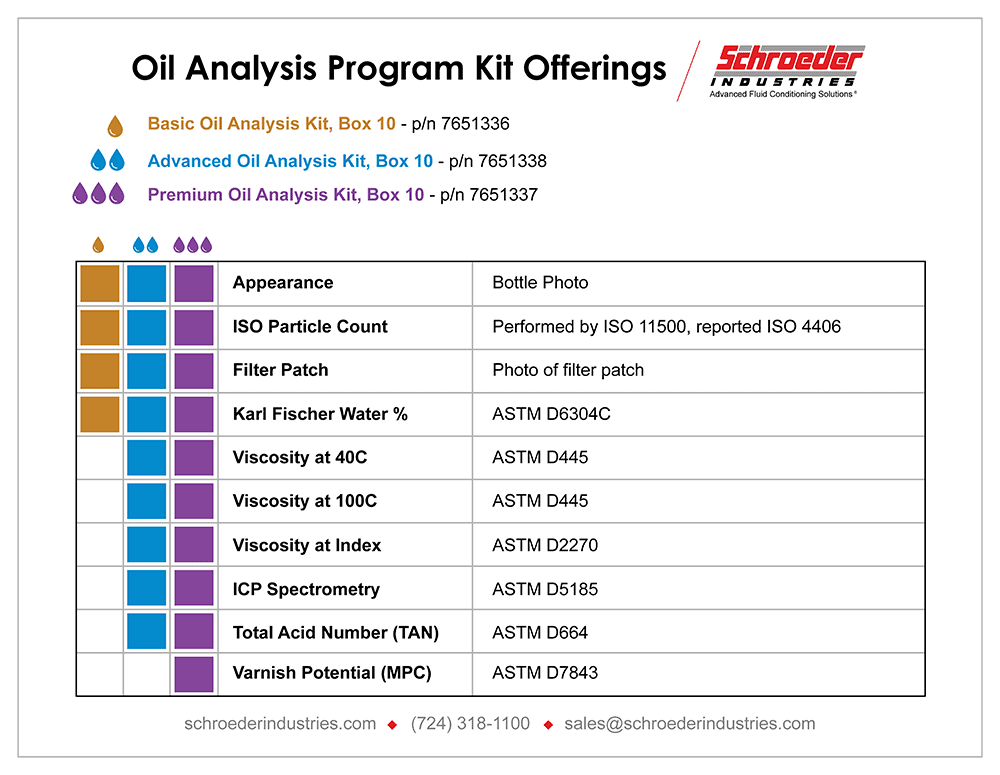
To satisfy virtually every application, Schroeder Industries offers several different test kit options, all backed by the powerful Fluid Care Portal.
Basic Analysis Kit
Our most cost-effective testing option, focusing on the most essential fluid condition factors.
Advanced Analysis Kit
Achieve deeper understanding of your fluid condition with a more expansive testing package.
Premium Analysis Kit
Our most comprehensive testing kit, for the most advanced insights into your fluid.
Below is a detailed breakdown of what the different Oil Analysis Program test kits offer.
How does the Fluid Care Portal enhance your fluid analysis program?
Regular testing is vital for monitoring trends in your fluid health and preventing problems before they arise. However, tracking results over time for many pieces of equipment takes time and hassle. As part of our testing and fluid analysis services, Schroeder Industries is now offering a smart digital solution for detecting trends in the quality of your hydraulic oil, diesel fuel, process water, and more.
Part of Schroeder Industries’ Oil Analysis Program, the Fluid Care Portal is a new, powerful digital tool for easily tracking the health of your equipment’s fluid as you test over time:
All your data is in one place, versus scattered over spreadsheets or various paper reports.
Easily monitor trends in fluid testing data over time, allowing you to detect and resolve contamination issues before they begin impacting your bottom line.
Monitor as many equipment assets as you need. Whatever the size of your operation, the Fluid Care Portal allows you to individually monitor the testing results for each piece of equipment.
Receive alerts when ISO Code, Water Content, or other parameters are exceeded. In the Fluid Care Portal, users can set target limit profiles for various parameters, creating customized criteria for your most critical components.
Comments Off on Marine Diesel Trouble? Fix Water Contamination Now!
Engine Failures Spell Danger
One of the most debilitating problems a vessel can face at sea is an unexpected loss of control. In rough seas, working engines can mean weathering the storm or succumbing to it. Shipping delays due to engine failures and repairs can have an impact on supply chains, and result in major disruptions and financial loss. More importantly, loss of control can have devastating consequences on crew and bystander safety.
When considering ways to prevent an unexpected loss of power for marine applications, controlling fuel contamination is an effective way to eliminate one of the greatest factors affecting diesel engine reliability today.
What Causes Fuel Contamination in Marine Applications?
Fuel systems in marine applications are vulnerable to water contamination due to the operating environment and liabilities in the fuel supply chain.
By virtue of operating at sea, on the coast, or in rivers, ships are exposed to high levels of humidity and water, which is the most common type of contamination that sea-going fuel systems face.
Diesel fuel is transported through a long network of refineries, bulk fuel suppliers, and dispensing stations before reaching its destination. At every stage, water, humidity, bacteria, pollen, and other contaminants can enter through open breathers, improperly sealed vessels, and other points of ingress.
Fluctuations in temperature can result in high levels of free water in a fuel system, which is more damaging than water that has dissolved into the fuel.
How Can Fuel Contamination Cause Engine Failure?
Contamination can affect engine operations in a variety of ways:
Buildup of bacterial sludge in the fuel due to water and bacterial contamination, also called diesel bug, can plug the engine filtration system and starve it of fuel
Small amounts of particulates and water can wear out an engine’s components over time, reducing its overall efficiency and eventually causing the engine to fail.
What Other Impacts Can Contamination and Contamination-Related Damage Have?
Besides total engine failure and its potential consequences, contamination has a range of direct and indirect impacts on equipment and operations:
Costly maintenance and repair of engines and equipment
Increased fuel-related expenses between acquiring clean fuel, disposing of contaminated fuel, and remediating/polishing contaminated fuel
Reduced fuel economy due to inefficiencies in the engine/high pressure common rail injection systems caused by contamination
Reduced engine and equipment longevity
Overall reductions in vessel or fleet profitability due to compounding expenses and downtime for repairs
How Can I Control Diesel Contamination?
Having a system in place to proactively monitor and prevent contamination where possible, plus a solution to remediate whatever contamination occurs, is key for controlling fuel contamination and protecting your engine.
Obtain fuel from a reputable source. Fuel is often contaminated before it enters a ship’s fuel system, but reputable suppliers who are familiar with contamination and take fuel cleanliness into consideration will provide higher quality fuel and prevent large, immediate influxes of contamination.
Ensure storage/fuel tank cleanliness. Before filling a fuel tank or bulk storage tank, be sure the tank is clean and dry.
Take precautions when transferring fuel/filling your system. Water and other contaminants are most likely to ingress during fuel transfer, so ensure that your transfer system is properly sealed.
Monitor the fuel quality levels of your storage tanks to determine the condition of the fuel being delivered to your engine and remediate or replace contaminated fuel before it can affect your equipment. Test kits such as Schroeder’s Diesel Fuel Quality Analysis Kits can provide important insights into the condition of your fuel, especially if you’re experiencing issues consistent with fuel contamination.
Closely monitor your fuel water separators and engine filters and empty them as often as needed. But remember: don’t rely solely on these separators and filters to completely resolve your contamination issues!
Acquire a fuel polishing system. A fuel polishing system/kidney loop attached to your system or to your storage tanks can help address contamination in real time.
Some degree of water contamination is inevitable, especially in a marine setting. However, proactive maintenance and preventative measures will significantly reduce your chances of catastrophic contamination-related equipment failure!
Schroeder Solutions for Diesel Contamination Control
Schroeder Industries understands all too well the negative impacts of fuel contamination. Our fuel filtration experts have developed a range of filtration products and services to maintain diesel fuel quality, with proven success in the maritime industry and beyond.
Here are just a few of our featured solutions:
BDFP – Bulk Diesel Filtration Panel
BDFP: Exceptional Quality, Turn-Key Stationary Fuel Filtration System
This simple-but-mighty filtration panel combines the power of our particulate GHPF filter and the exceptional water removal capabilities of our coalescing GHCF filter to defend against particulate and water contamination.
With an integrated pump, the BDFP is ready to use without requiring a new pump purchase for the filter panel.
The streamlined BDFP design is easy to integrate into new and existing fuel storage systems, and the minimal element change clearance makes maintenance easy.
Flow Rating (Electric Motor Option):
14 gpm or 25 gpm (53 or 95 L/min)
Flow Rating (Air-Operated Option):
16 or 25 gpm (53 or 95 L/min)
Ambient Temperature Range:
32°F to 104°F (0°C to 40°C) Standard; -20°F to 140°F (-29°C to 40°C) Heater Option
BDFP Prevents Water Contamination-Related Engine Failures in Workboat Fleet
When a fleet operator in the Mississippi River region launched a new pushboat with a brand new engine, the pushboat experienced sudden engine failure just a single mile into its maiden voyage.
Analysis revealed water contamination in the fuel source as the primary cause of this failure. When the customer approached Schroeder Industries for help, our experts recommended a kidney loop setup featuring the BDFP to ensure fuel quality, reduce engine maintenance, and protect against further costly, dangerous failures. Its performance was so outstanding that the customer implemented the BDFP across their three fleets.
Here’s how the BDFP helped this customer save money and protect their assets!
Reduced Downtime & Maintenance
Eliminated Contamination-Related Engine Failures
Prevented Major Engine Repairs (Saving Up To 100K+)
Schroeder’s particulate GHPF filter and coalescing GHCF filter combine for exceptional defense against particulate and water contamination. With the option of adding a second GHCF in parallel on the BDF, flow rate and coalescing capabilities can be doubled!
This compact filter excels in marine applications, fleet and mobile vehicle applications, railroad applications, and much more!
Flow Rating:
BDF1: up to 25gpm (95 L/min) BDF2: up to 50gpm (189 L/min)
Max Operating Pressure:
150 psi (10 bar)
Temperature Range:
w/ water sump heater: -20°F to 225°F (-29°C to 107°C); w/out heater: 32°F to 225°F (0°C to 107°C)
Due to poor fuel quality, a Class 1 Rail Carrier was experiencing frequent in-field failures of their MOW (Maintenance-of-Way) equipment, including their Fuel & Lube Trucks.
This lack of fuel quality control was costing the customer thousands of dollars in parts and labor, downtime, and lost revenue overall. Schroeder’s experts retrofitted the customer’s MOW fleet with BDF2 filters (BDF with dual GHCF filters), providing immediate improvements.
Here’s how the BDF2 helped this customer save money and protect their assets!
57% Increase in Particulate Filtration Efficiency
19% Reduction in Absolute Water Content (52ppm Below World Wide Fuel Charter Maximum Water Content)
BestFit® Elements: Superior Coalescing & Particulate Filtration
With options for both coalescing and particulate filtration and all the advantages of Schroeder’s powerful filter element technology, the BestFit® series provides improved diesel filtration performance.
SBFC element uses patented, three stage coalescing filtration technology
Synthetic filtration media eliminates degradation due to high water content fuel
Use of stainless steel support structure and polymer components prevent corrosion from high water content exposure
Direct fitment into existing installations allow for immediate performance improvements with no modifications
Differential Pressure Rating:
75 psid
Max. Operating Temperature Range:
225°F (107°C)
Filtration Rating:
225°F (-29°C to 107°C); w/out heater: 32°F to 225°F (0°C to 107°C)
BestFit® Elements Stabilize Inventory Crisis & Improve ROI
An oil & gas drilling contractor struggled to source a critical diesel fuel filter element required on all their job sites, resulting in company-wide operational impacts.
Not only was Schroeder Industries able to provide a seamless transition and stable supply of vital elements using our BestFit® Element series: The BestFit® Elements ended up outperforming the drilling company’s previous elements!
Here’s how BestFit® Elements improved ROI and helped this customer’s business return to smooth sailing!
Element Inventory & Supply Stabilized
Increased Service Life of Filter Elements vs. Previous Elements
Competitive Price Point & Improved Element Performance Provided Immediate ROI Increases
Damp, Dirty Diesel Deals Damage: Fix It with Fuel Filtration Solutions from Schroeder Industries!
Our experts can help you monitor and decontaminate your marine vessel fuel supply and prevent the costly, potentially dangerous effects of water contamination and more. Contact us for a consultation, quote, or more information!
Contact-Blog-Water Contaminated Diesel In Marine Applications: Fix It With Filtration!
Comments Off on Unlock Peace of Mind: Prevent Water Contamination Fast
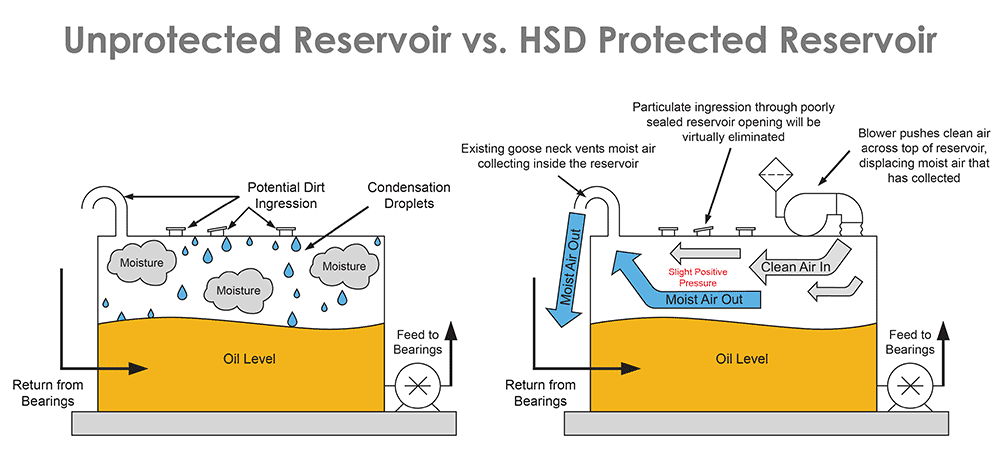
Most hydraulic reservoirs in major industries including pulp & paper, primary metals, and more feature a pocket of open space between the fluid level and the top of the reservoir. This open space, known as head space, fills with moisture as humid air ingresses via faulty seals, vents, and other entry points.
As the moisture builds in the head space, water condenses at the top of the reservoir, eventually coalescing and falling into the oil.
This water contamination can cause a range of serious problems which can impact your equipment’s efficiency and may require repairs, including:
Rust
Cavitation
Sensor failures
Reduced oil lubricity
How Schroeder’s Head Space Dehydrator Helps:
Dewatering units such as the Triton Dehydration Stations are excellent for targeting water contamination when oil has already become saturated, but preventing contamination before it reaches critical levels is ideal.
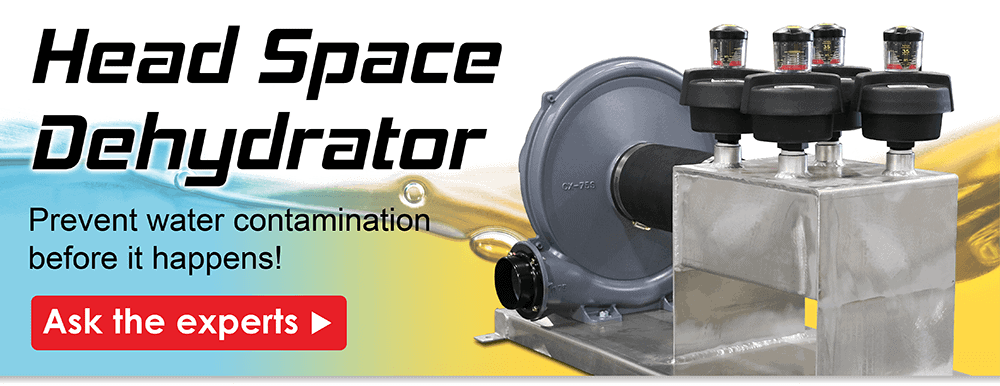
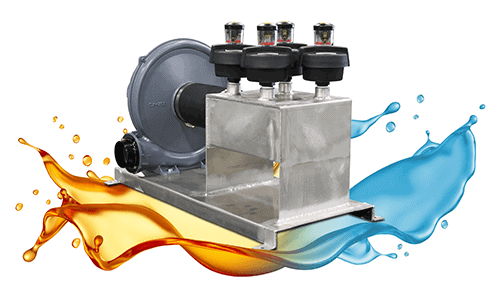
The new Head Space Dehydrator is designed to combat moisture in the head space of a hydraulic reservoir before it contaminates the oil. This unit is permanently installed on a hydraulic reservoir so that humidity inside the reservoir can be managed continuously.
Here’s how it works:
The Head Space Dehydrator assembly pulls ambient air into the chamber through a series of particulate breathers.
The clean, dry air is then blown through the head space above the fluid level, displacing and venting the moist internal air though existing ventilation points.
As the moist air is displaced, the opportunity for water contamination via condensation is reduced.
Specifications:
Flow Rating:
Max flow rate 282 cfm (7985 lpm)
Blower:
1/2HP blower with 220-275/380-480V-60Hz-3 phase motor
Breathers:
Uses 4 breathers which include -0.5 psi (-0.035 bar) differential pressure indicators
Features & Benefits
Cost effective, reliable solution for water ingression
Improved oil cleanliness
Increased lifespan of oil and components
Markets & Applications
Ideal for industrial applications where water contamination may be introduced to the reservoir head space, particularly:
Steel & Primary Metals
Pulp & Paper Production
Bulk Storage
and more!
Ask the experts at Schroeder what the HSD can do for your application!